Plasma–TIG Longitudinal Seam Welding Machine
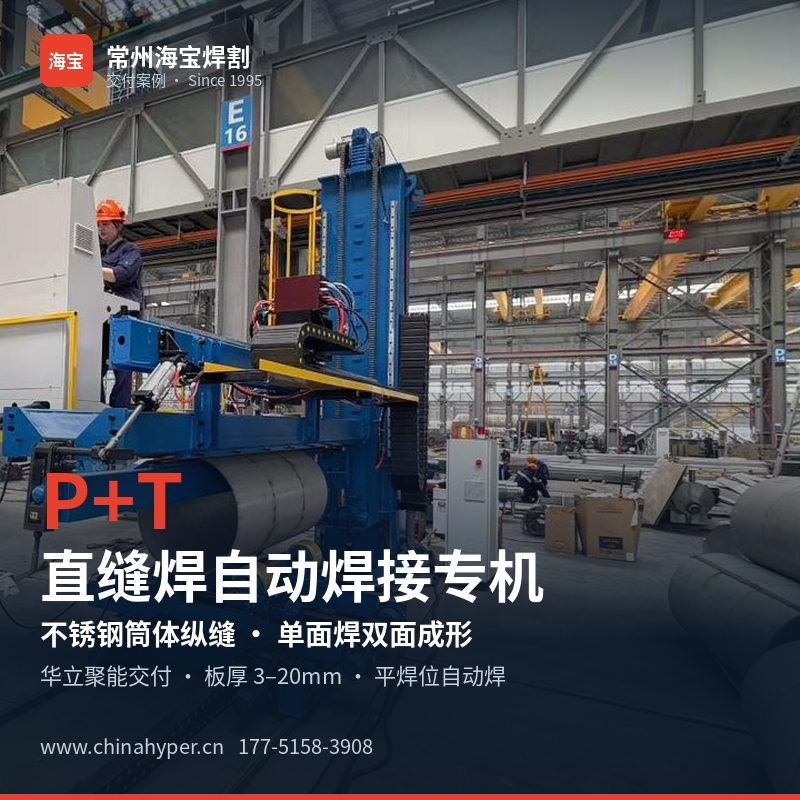
The haibao robot P+T longitudinal seam welder combines plasma and TIG welding with a column-and-boom arrangement, cross-slide adjustment, rail travel and turning rolls. The reference delivery at Wuxi Huali Juneng addresses long shell seams in tank and pressure-vessel fabrication.
Equipment and application images
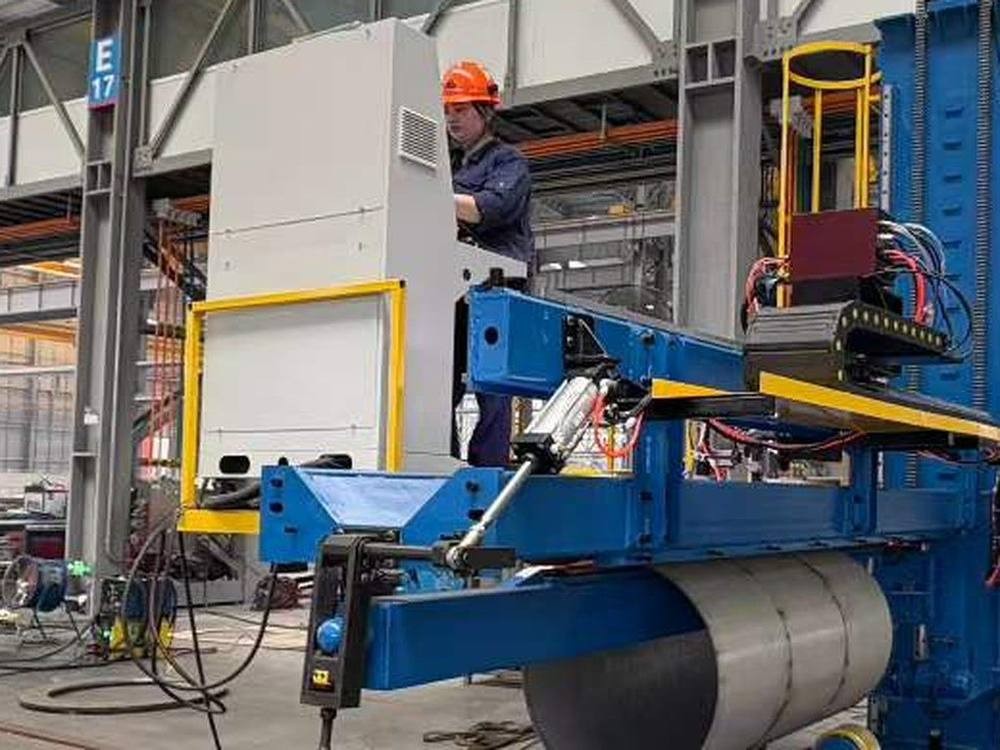
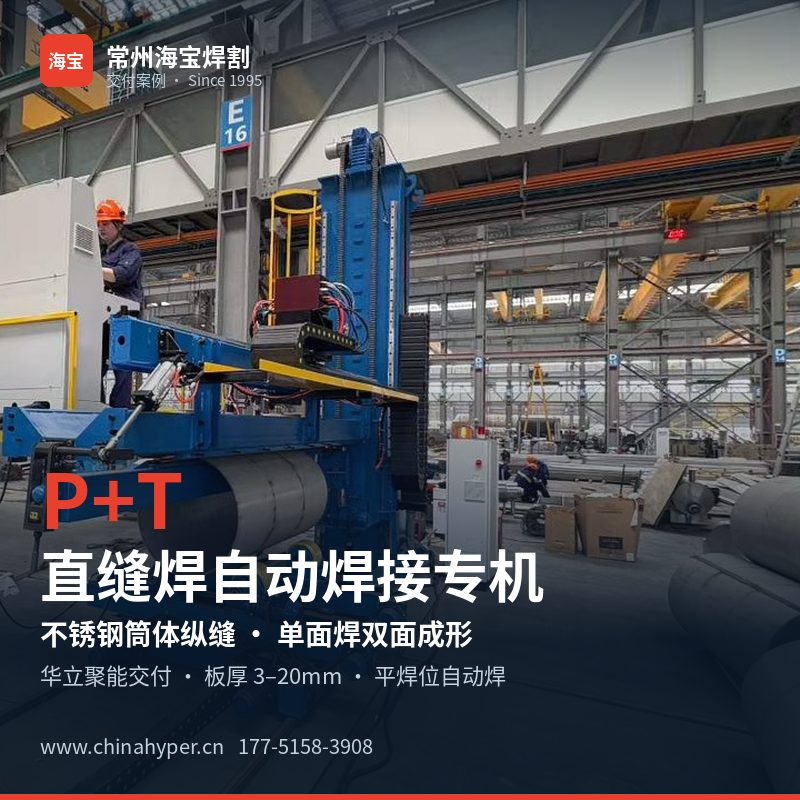
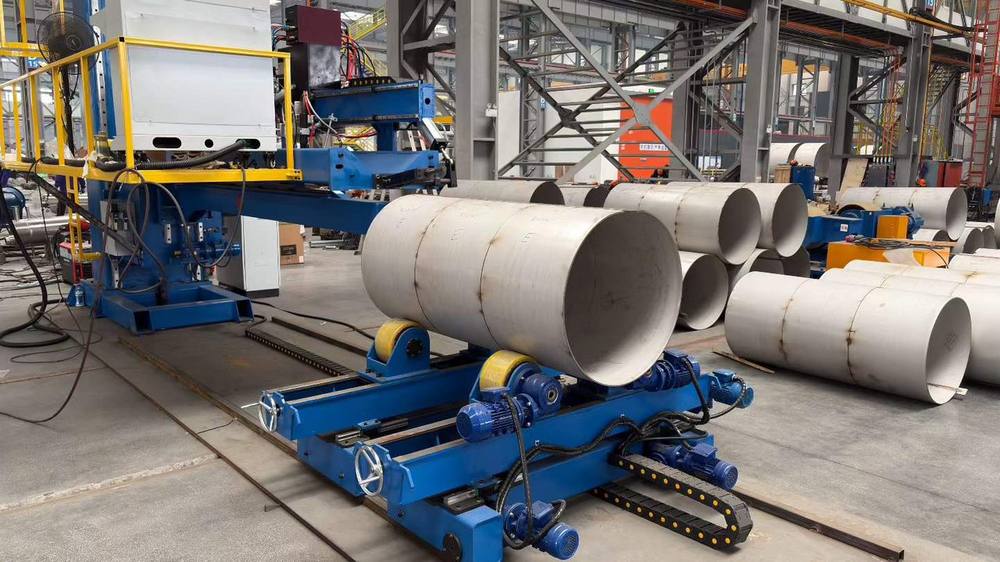
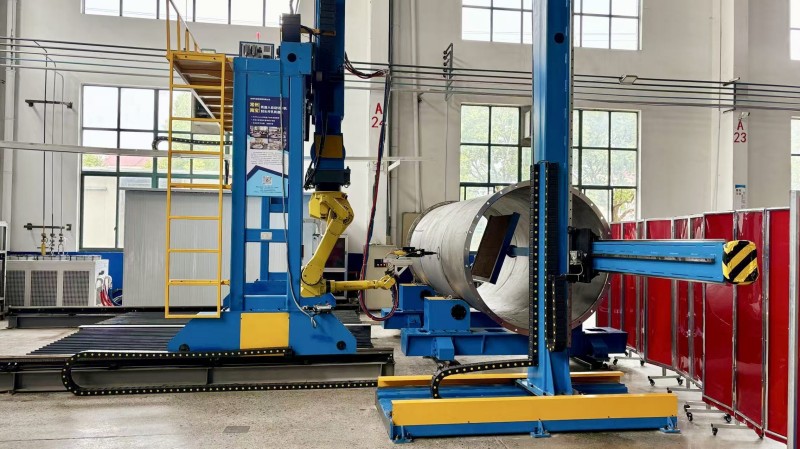
Plasma–TIG longitudinal seam welding system reference |
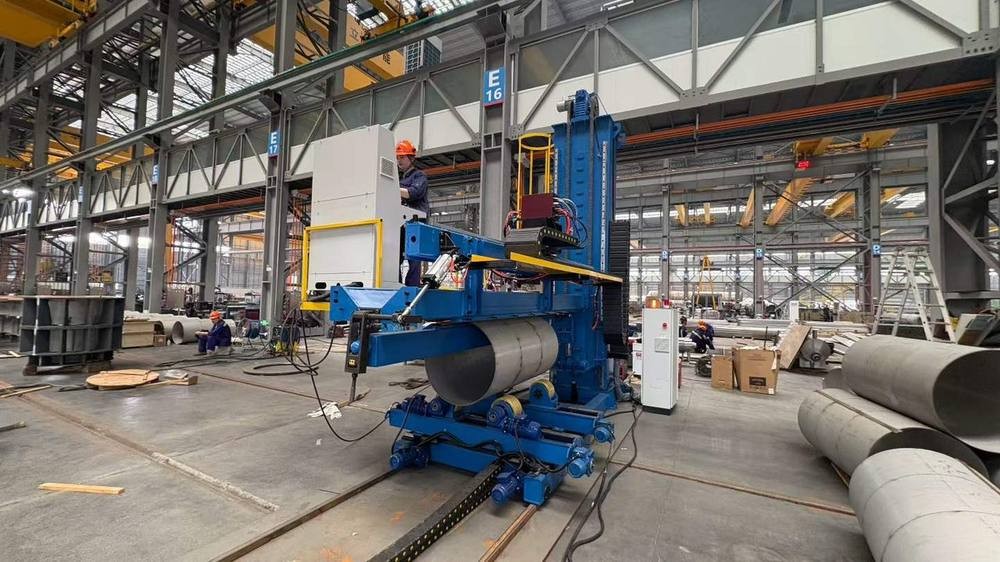
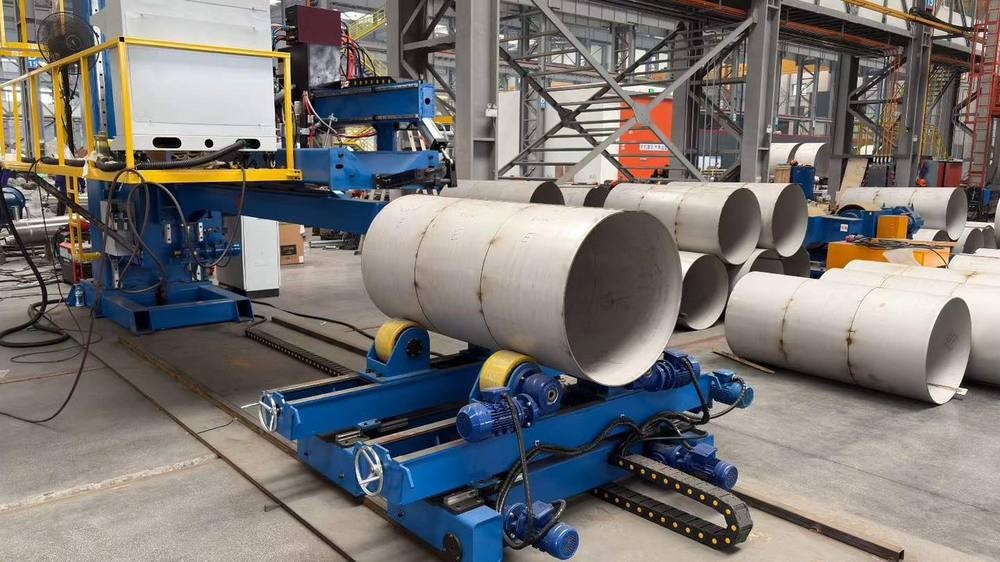
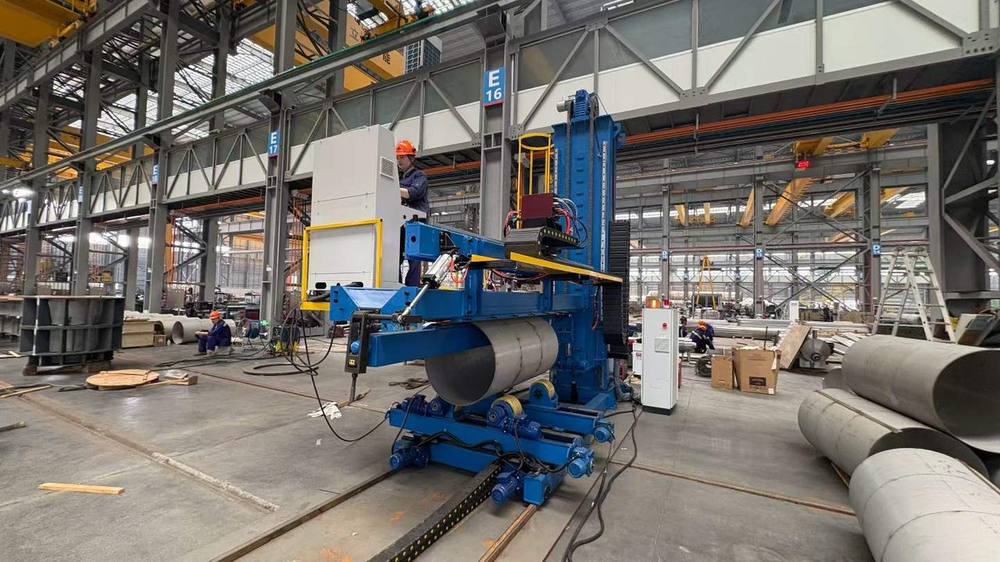
Complete welding installation at Huali Juneng |
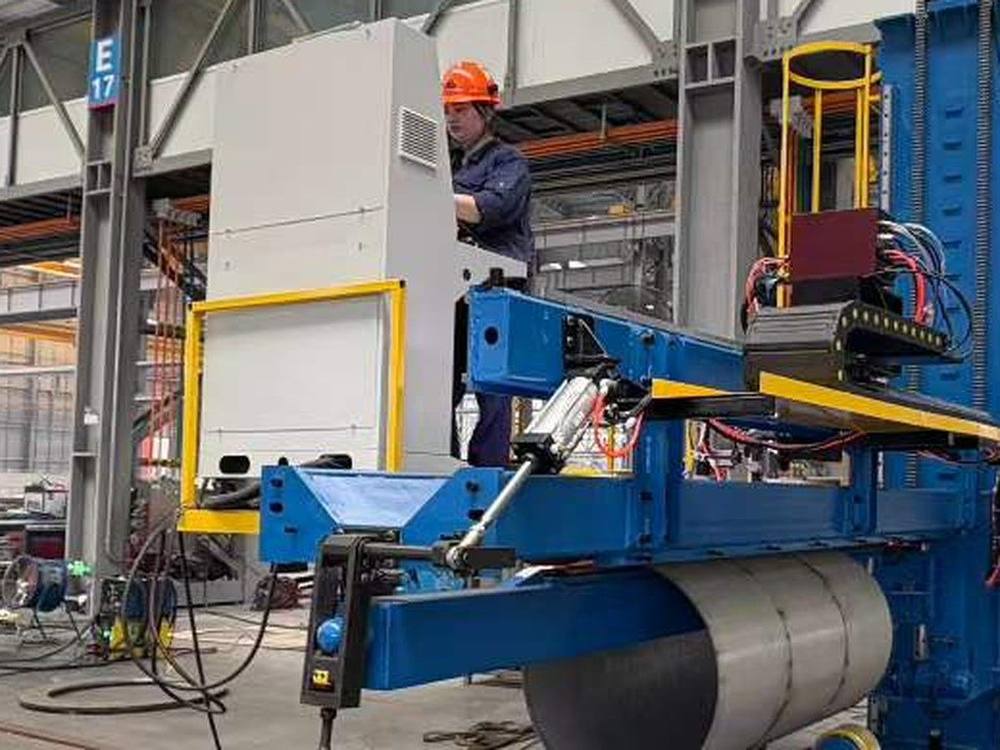
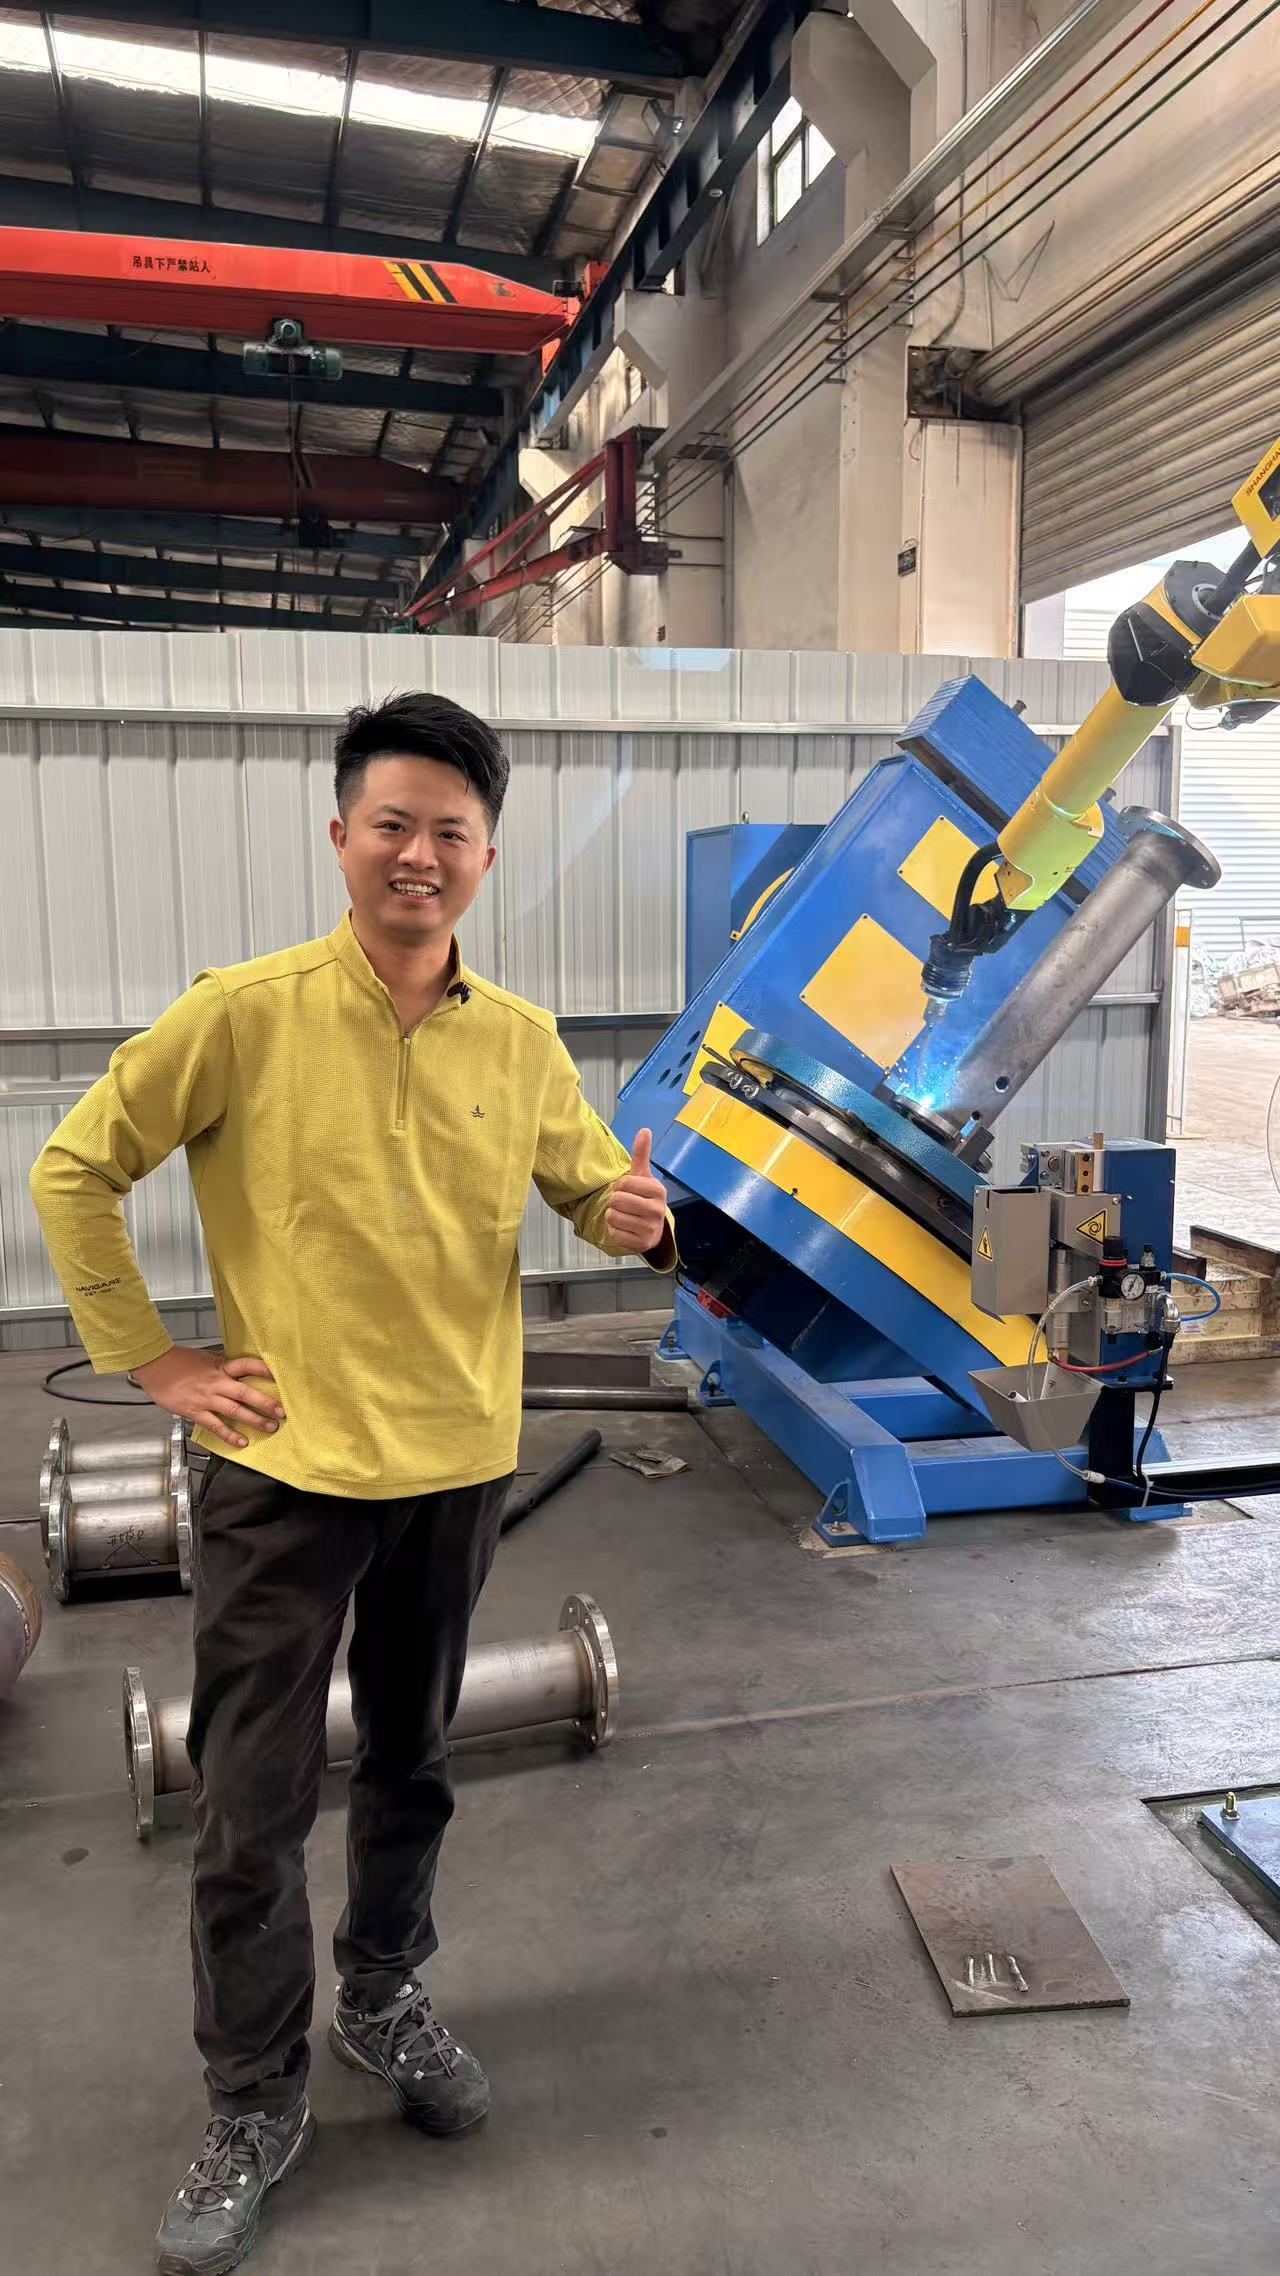
Integrated welding power and control cabinet |
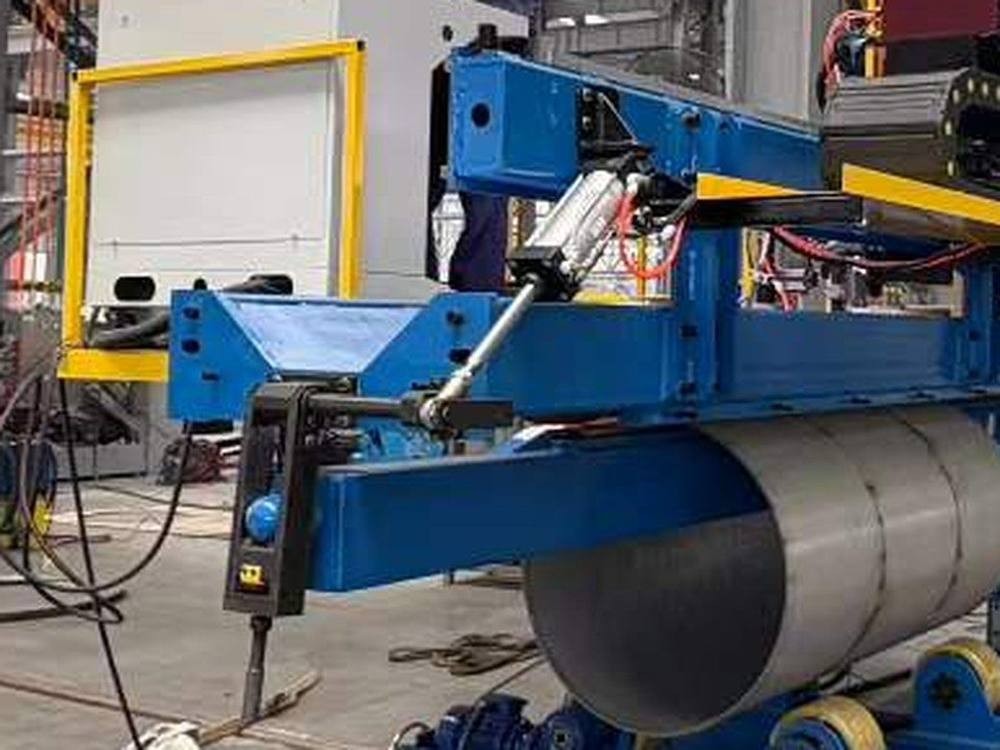
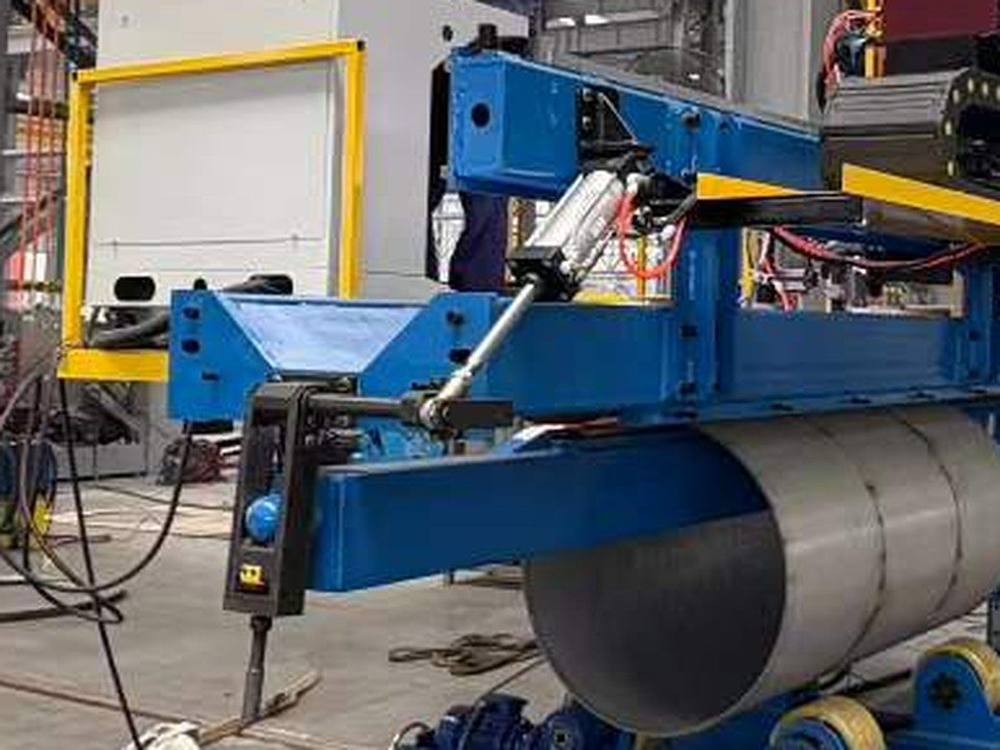
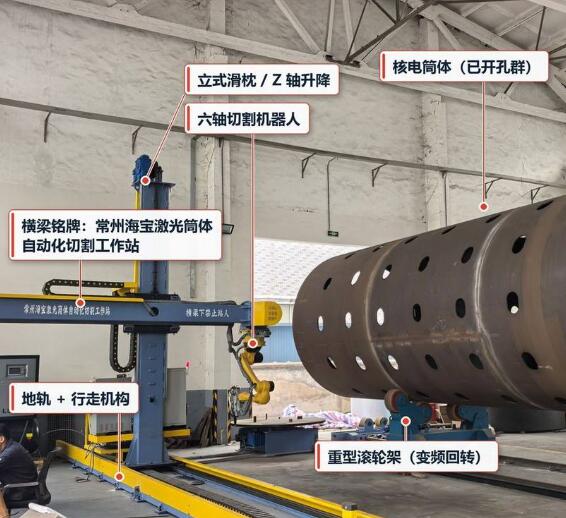
Cross slide and P+T torch aligned with the shell seam |
Welded stainless shell and turning-roll station |
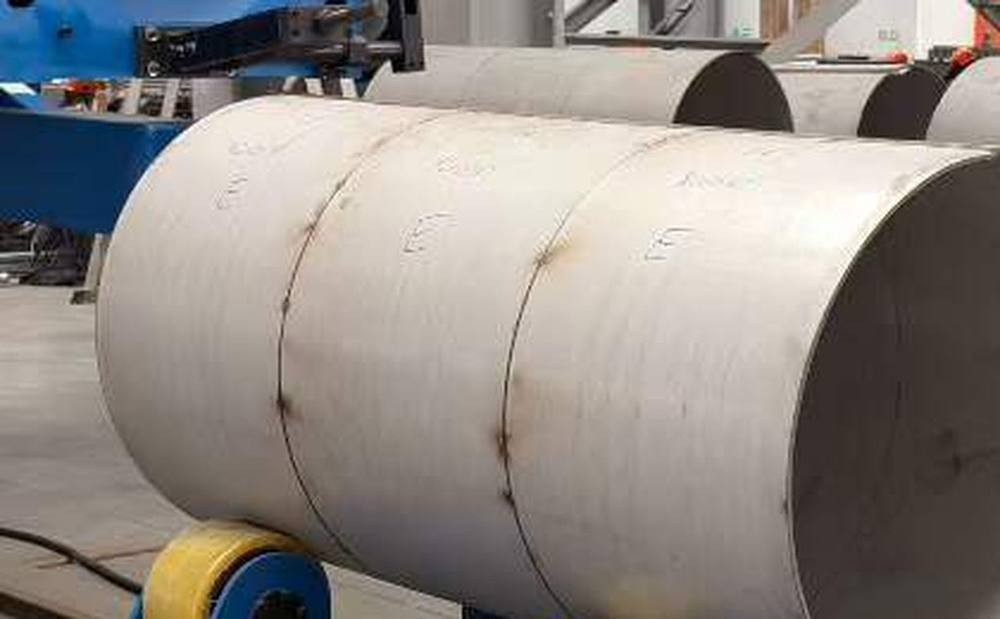
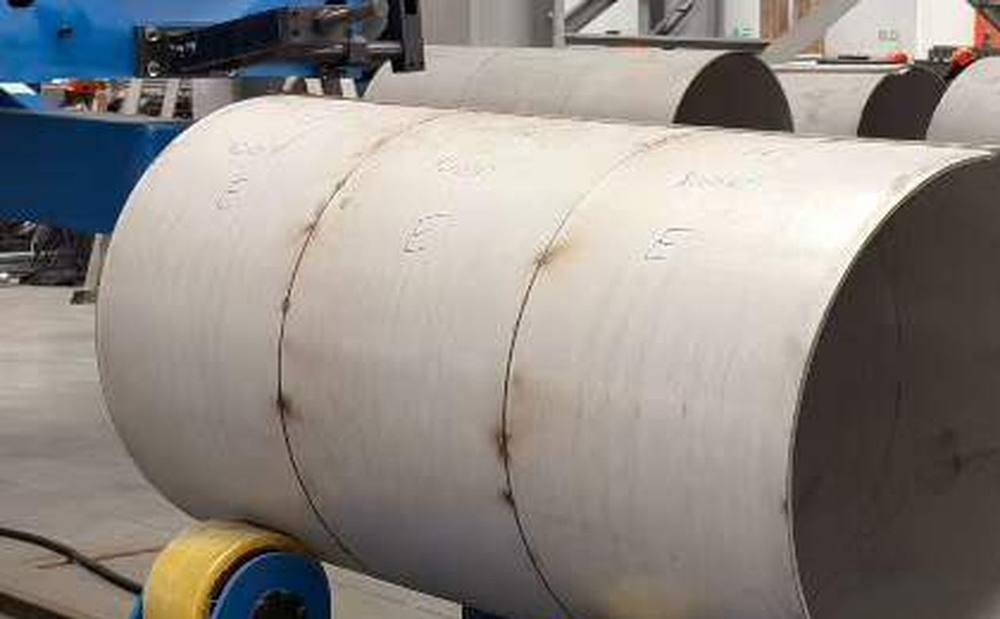
Close-up of the longitudinal weld profile |
haibao robot · PRESSURE VESSEL PRODUCTION EQUIPMENT
Automatic Longitudinal Seam Welding for Stainless Steel Shells
The haibao robot P+T longitudinal seam welder combines plasma and TIG welding with a column-and-boom arrangement, cross-slide adjustment, rail travel and turning rolls. The reference delivery at Wuxi Huali Juneng addresses long shell seams in tank and pressure-vessel fabrication.
Keep the seam in a controlled position
The turning rolls support the shell and bring its longitudinal joint to the required welding position. The cross slide aligns the torch, while controlled travel follows the seam. The column and boom provide the reach and height adjustment needed for the specified shell range.
Plasma penetration and TIG weld formation
In the described P+T process, the plasma stage provides penetration and TIG contributes to the finishing stage. One-sided welding with reverse-side root formation is possible within a validated joint window. Gap, mismatch, edge preparation and shielding conditions are established through welding trials.
Recipes and changeovers
The control package stores the settings for the approved material and joint combinations. Changing shell dimensions may also require support adjustment, fixture checks and alignment. Stored recipes improve repeatability but do not replace checking incoming parts against the qualified fit-up limits.
A process window, not one universal thickness claim
The source gives a configurable 3–20 mm material range and several seam lengths and roll capacities. The actual welding procedure, number of passes and need for a bevel depend on the material and joint. Factory and site trials define the agreed production window and inspection results.
Configuration reference
| Process | Plasma arc welding + TIG; individual or combined configuration |
| Typical materials | 304/316L stainless steel; other grades by process review |
| Thickness reference | 3–20 mm; joint-specific procedure validation required |
| Seam length options | 2,000 / 3,000 / 6,000 mm; custom lengths by review |
| Shell diameter reference | 300–3,000 mm; larger configurations by review |
| Travel speed range | 50–1,000 mm/min equipment range; welding speed set by procedure |
| Turning-roll options | 5 / 10 / 20 t, selected for the complete supported load |
| Controls | PLC and touchscreen with stored process recipes |
| Reference power supply | 380 V, 50 Hz; destination supply confirmed in the proposal |
Discuss your application
Send material, thickness, shell diameter, seam length, joint drawing, inspection requirements and output target. We will review the welding route, support capacity and sample-weld plan.
haibao robot
Shao Yicheng · Key Account Project Director · International Welding Engineer (IWE)
Email: masterhyper@163.com
Phone / WhatsApp: +86 177 5158 3908
Office: +86 519 8837 0688
Explore welding and cutting equipment · Read more application stories
INQUIRY
Categories
Latest News
Contact Us
Contact: Mr.Shao
Phone: 0086-17751583908
E-mail: 691043690@qq.com
Whatsapp:86-17751583908
Add: shanghai, China TianHe District, GuangZhou Num 899