Flat Plate Seam Welding Machine
Automatic flat plate butt welding for tank and pressure vessel fabrication. Piano-key clamping and controlled torch travel, with TIG, MIG/MAG, plasma or SAW configurations selected for your material and joint.
Equipment and application images

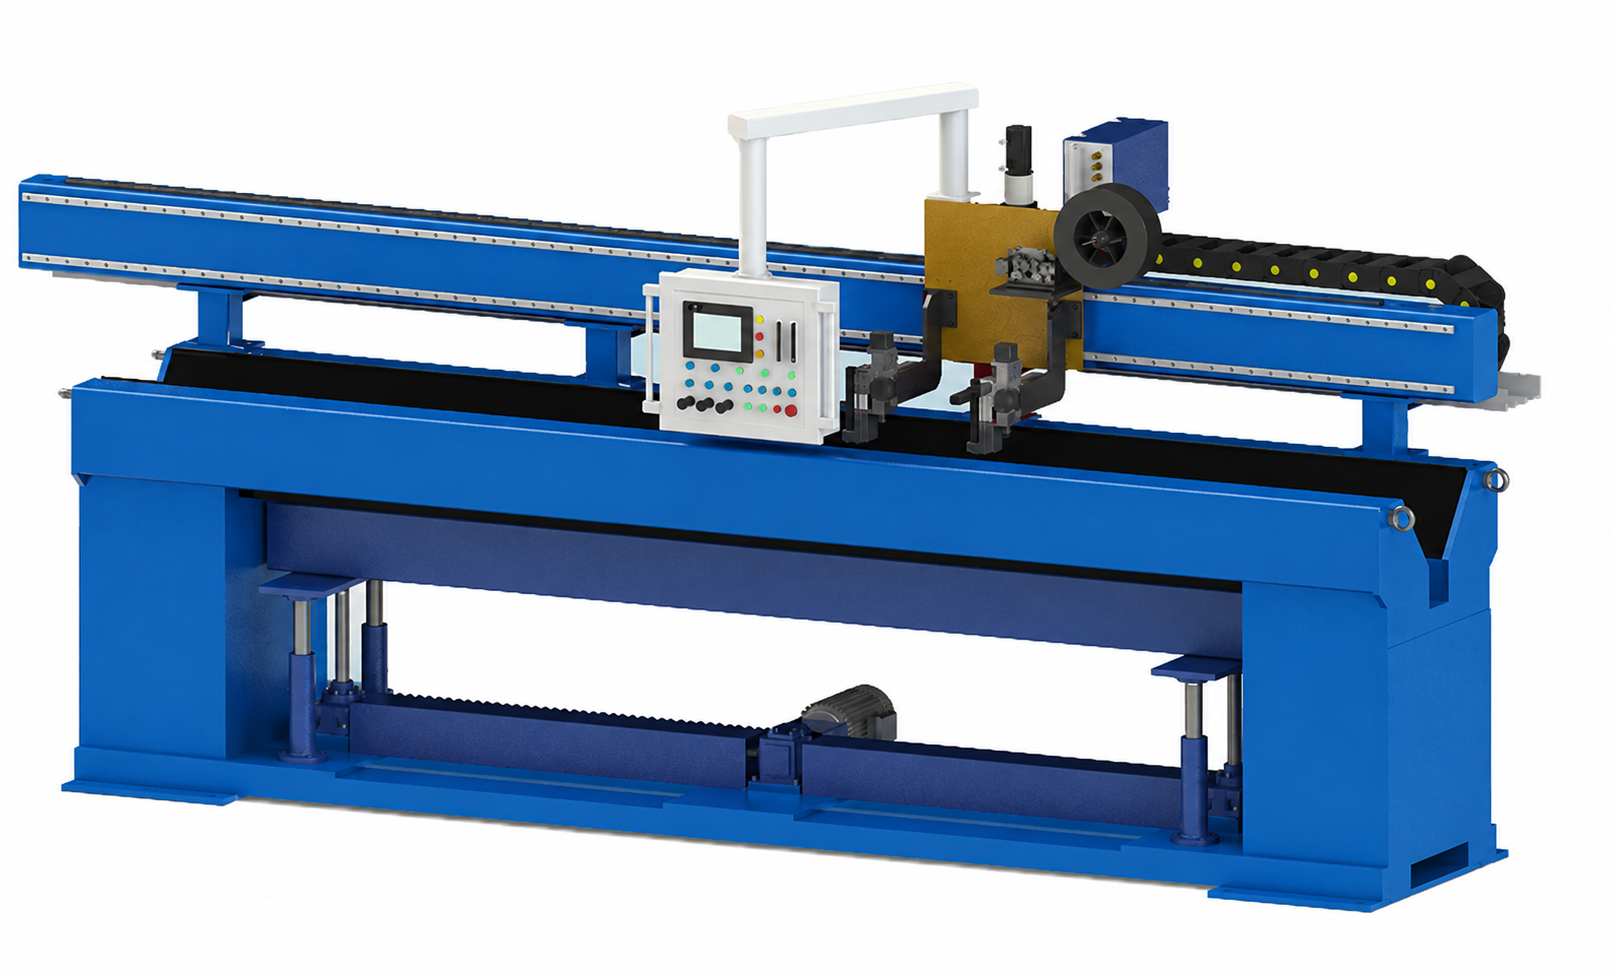
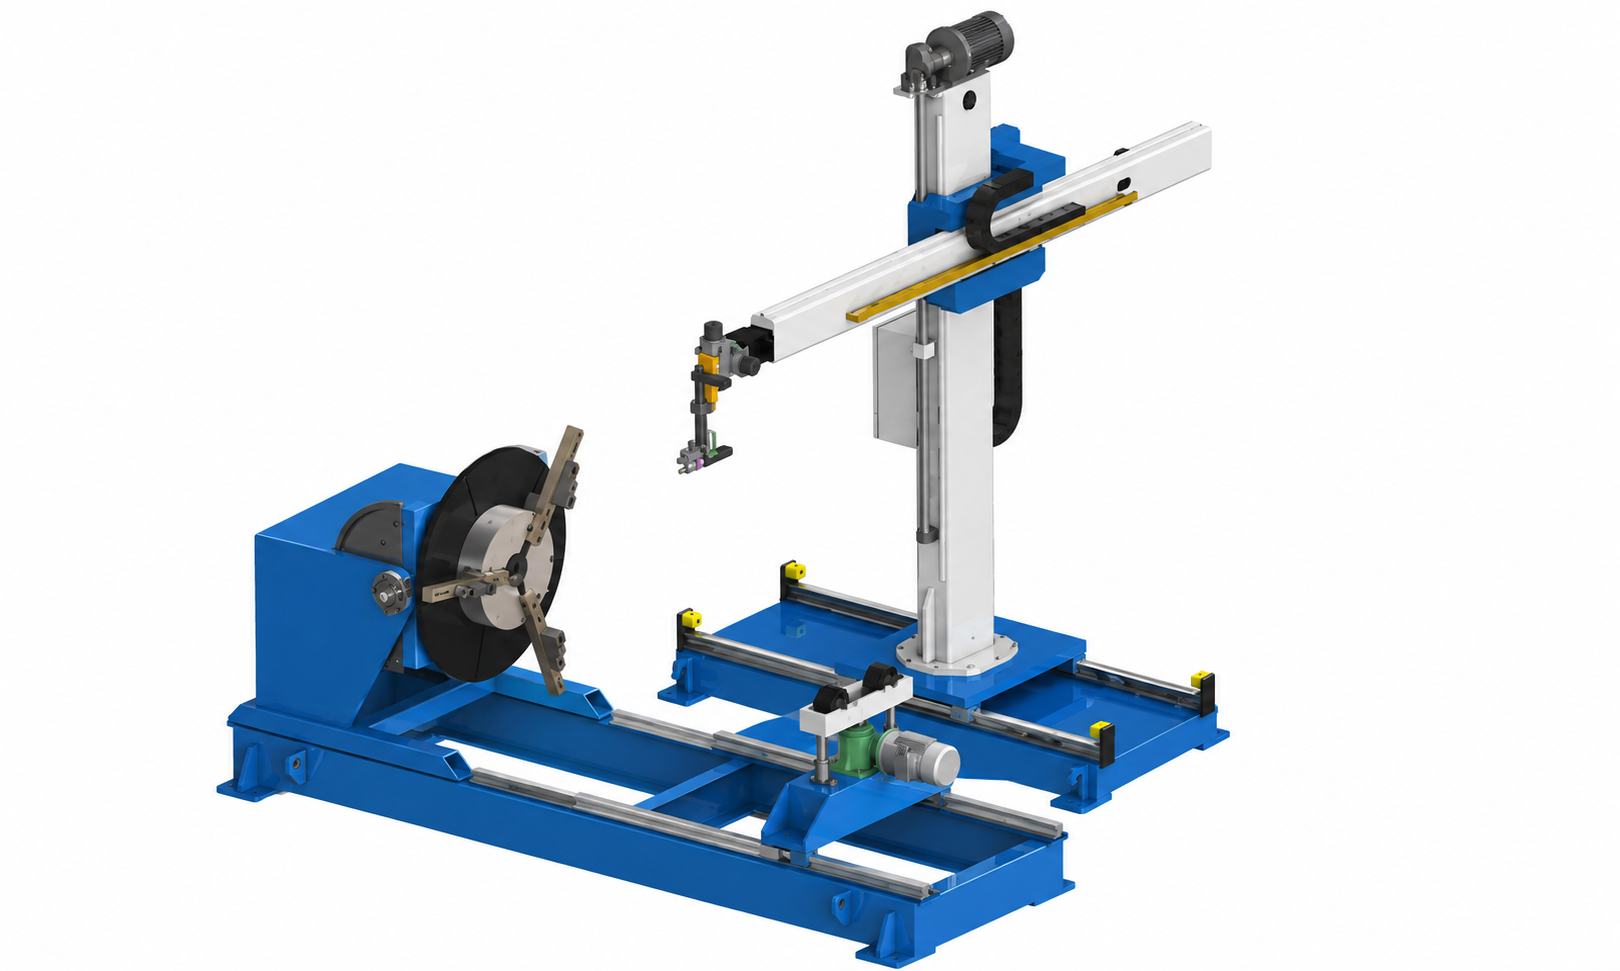
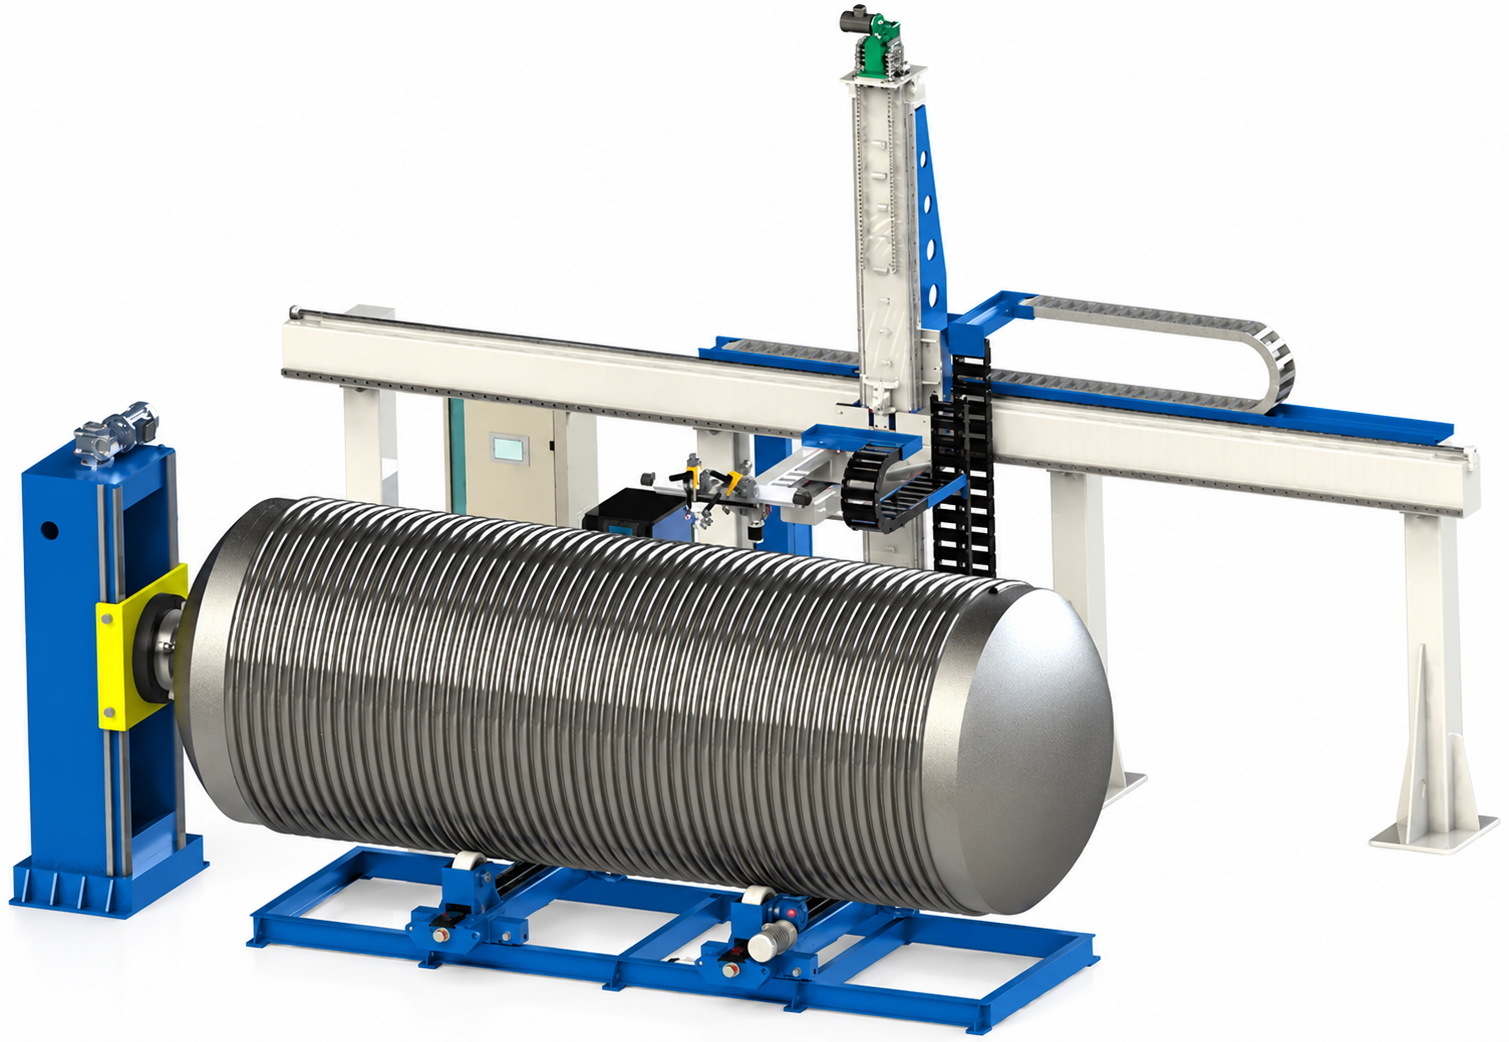
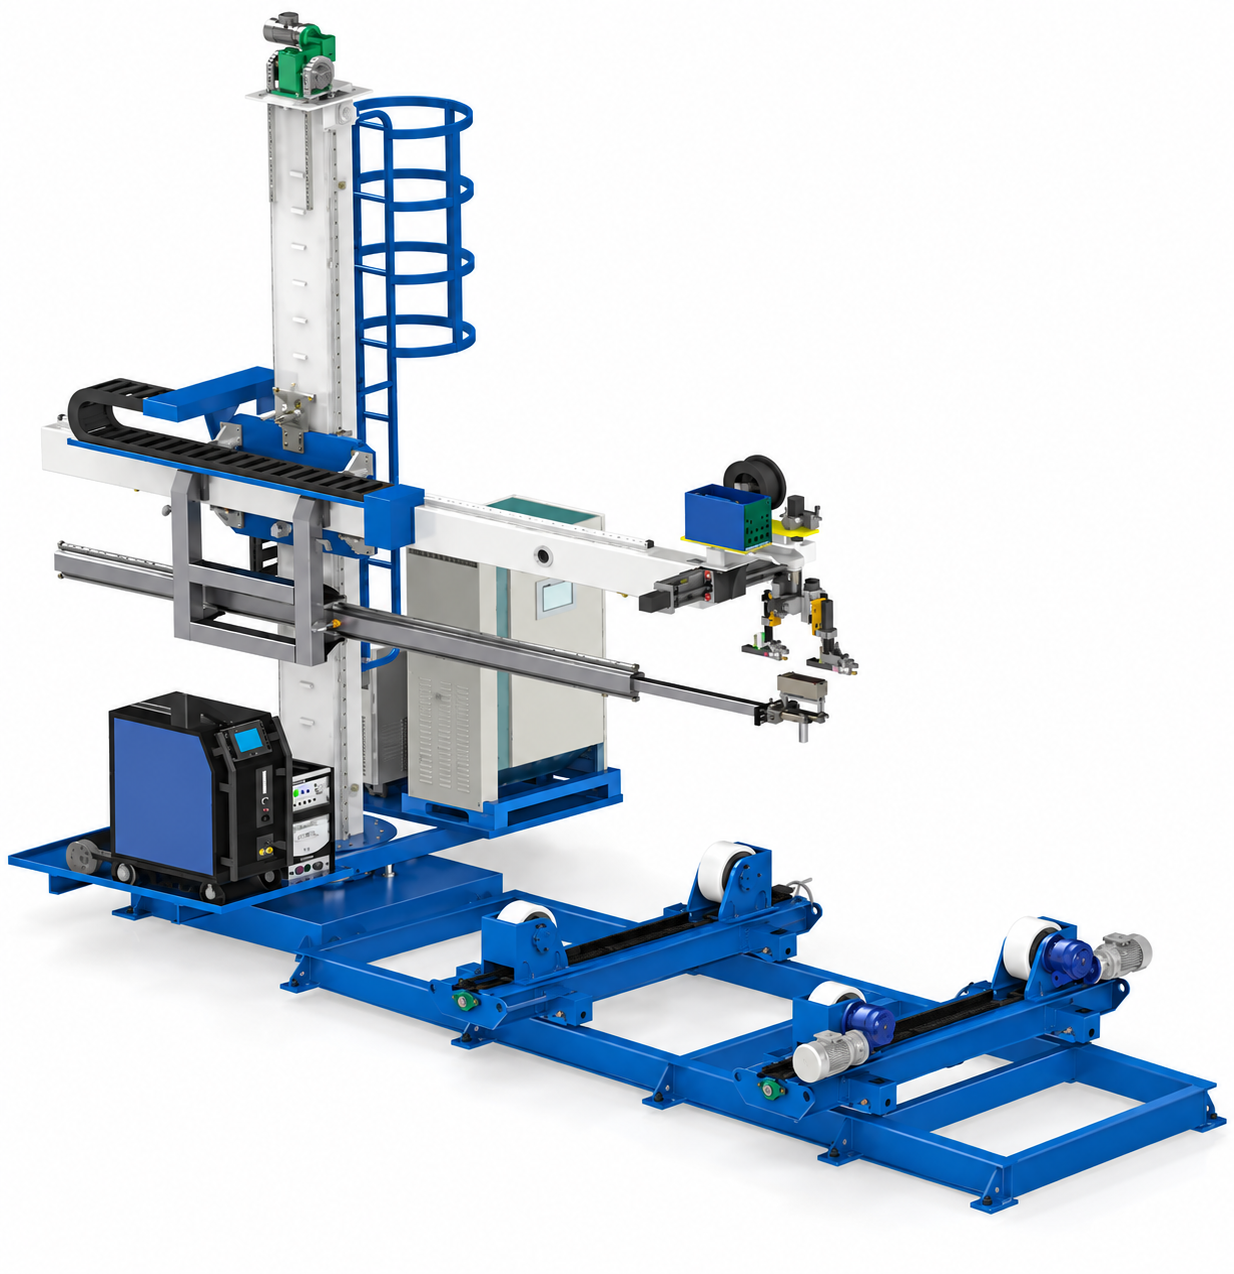
CAD configuration illustration. Final equipment follows the agreed technical scope.

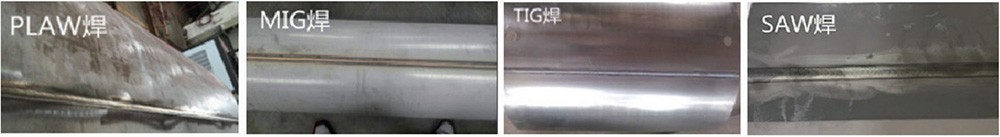
Welding application reference. Results depend on material and welding procedure.
Automatic flat plate butt welding for vessel fabrication
The haibao robot flat plate seam welding machine holds adjoining plate edges with piano-key clamps while a powered carriage guides the welding torch along the joint. It is designed for straight butt seams in plate preparation for tanks, pressure vessels and sheet fabrication.
Choose the welding process for your plates
TIG (GTAW), MIG/MAG (GMAW), plasma arc welding (PAW) and submerged arc welding (SAW) are application-dependent options. The power source, torch, backing arrangement and shielding system are selected for your material, thickness and required weld quality. These processes are alternatives, not a claim that one standard configuration performs all of them.
Working range
| Configuration | 3 m class | 6 m class | 8 m class | 10 m class |
|---|---|---|---|---|
| Single-torch effective weld length | 3,200 mm | 6,160 mm | 8,160 mm | 10,160 mm |
| Dual-torch effective weld length | 2,700 mm | 5,700 mm | 7,700 mm | 9,700 mm |
| Plate thickness selection range | 1–12 mm | 2–12 mm | 2–12 mm | 2–12 mm |
Nominal carriage speed: 60–1,200 mm/min. Adjustable clamping-finger spacing: 10–40 mm. Motorized backing adjustment: 60 mm. Final welding capability depends on the selected process, material, joint preparation and qualified procedure; the thickness range is not a single-pass guarantee.
Clamping and controlled travel
The piano-key arrangement supports plate alignment and restrains the joint during welding. Adjustable fingers and a backing system allow the fixture to be matched to different workpieces. Stable carriage motion helps maintain a consistent travel speed along long plate seams.
Typical applications
Flat plate butt seams before tank or vessel shell forming.
Stainless steel and carbon steel fabrication.
Long, straight seams requiring repeatable torch positioning.
Other materials, including titanium and aluminum, require a specifically matched process and fixture arrangement. Ask us to review the material grade and joint drawing.
Frequently asked questions
Is this the same as a cylinder seam welder?
This configuration is intended for flat plates. Cylindrical shells require a suitable mandrel, loading clearance and shell support. Send a drawing so we can recommend the correct fixture.
Can the machine weld without a bevel?
That depends on material, thickness, fit-up and welding process. A sample welding trial and the acceptance criteria should establish the procedure before production.
Request a configuration and quotation
Send haibao robot your plate material and grade, thickness range, maximum weld length, plate width, joint drawing, daily output and weld inspection requirements. Include the preferred process and available power supply. We can then review the clamping layout, welding package and loading method with you.
Contact haibao robot about your plate welding application
INQUIRY
Categories
Latest News
Contact Us
Contact: Mr.Shao
Phone: 0086-17751583908
E-mail: 691043690@qq.com
Whatsapp:86-17751583908
Add: shanghai, China TianHe District, GuangZhou Num 899