News
Half-Pipe Jacket TIG Welding: Jinzong | haibao robot
Project photographs and equipment references
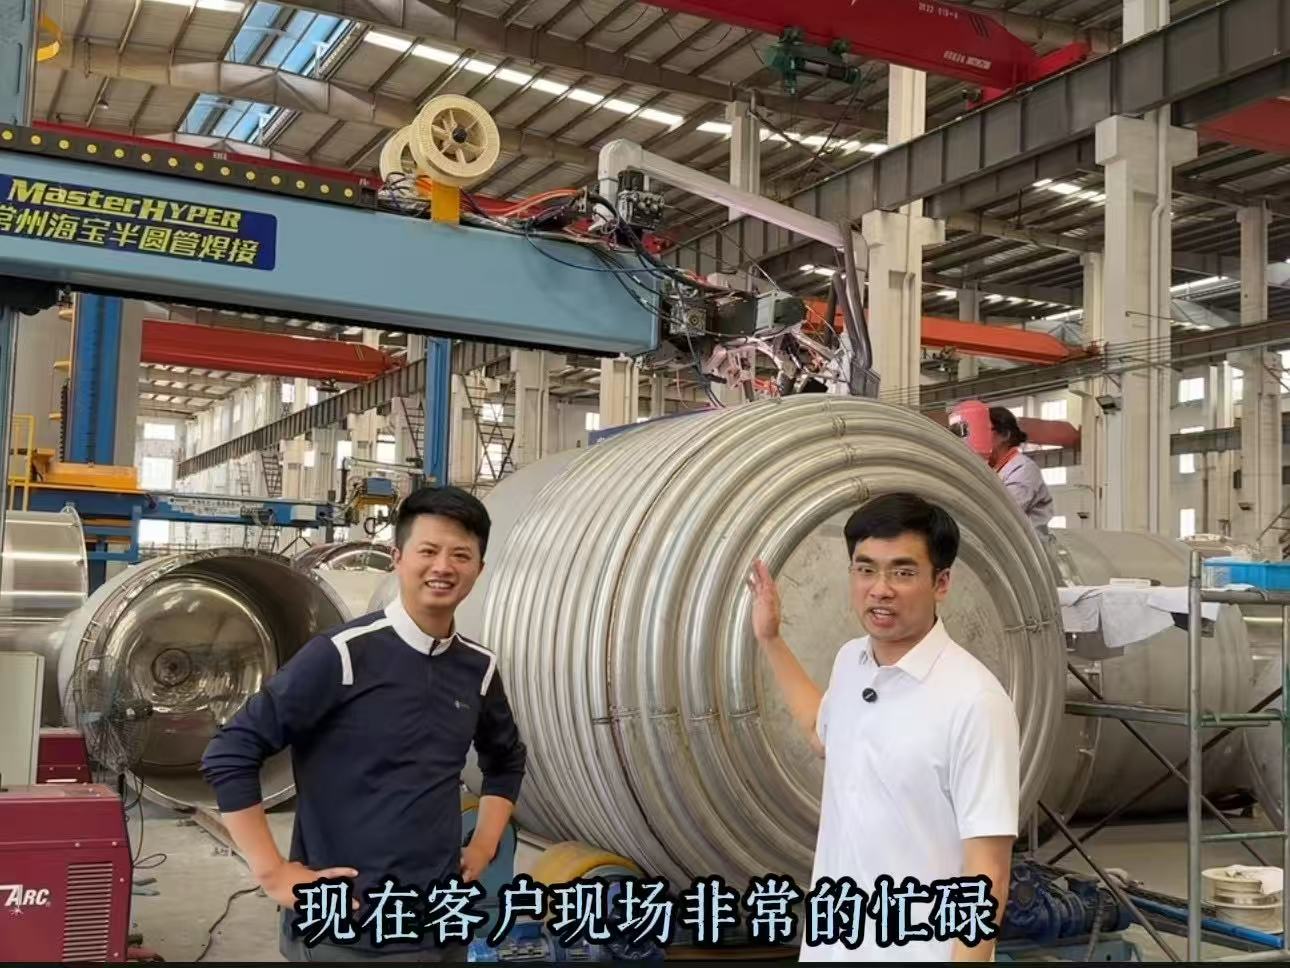
Half-pipe jacket welding at the Guangdong Jinzong workshop |
haibao robot · CUSTOMER APPLICATION
Automated Half-Pipe Jacket TIG Welding at Guangdong Jinzong
In 2026, haibao robot supplied Guangdong Jinzong Machinery with an automatic half-pipe TIG welding system for reactor fabrication. The project addresses long spiral seams on vessel shells and transitions toward the heads.
Why jacket welding becomes a bottleneck
The torch must follow a spiral path as the vessel rotates. Thin stainless half-pipe sections are sensitive to heat input and shielding, and long welds make consistency across shifts difficult. Jinzong needed more predictable production scheduling, repeatable weld quality and simpler changeovers.
Coordinated rotation, feed and tracking
The documented system combines a column-and-boom welding unit, heavy-duty rotators, vision-based seam location, laser seam tracking, a digital TIG source and PLC controls. Rotation and axial torch feed generate the spiral path; the tracking system corrects position variation. A profiled pressure roller helps maintain contact between the half-pipe and shell.
Workpiece and configuration review
The published configuration range includes shell diameters of 800–3,200 mm, lengths up to 6,000 mm and half-pipe sizes of 76, 89 and 108 mm. Material options include 304/316L stainless steel, carbon steel and duplex steel. Rotator capacity, torch arrangement and process options are selected against the actual workpiece and technical agreement.
Operating sequence
Load and align the vessel, select its stored parameter group, locate the seam and apply the pressure roller. The system starts the weld, coordinates spiral motion, uses separate transition settings where required and completes the crater-fill sequence before unloading. Recorded process data supports production review alongside the specified inspection results.
Results reported for this application
The project report describes a reduction from 3–5 days of manual half-pipe welding to less than one day per reactor, with one operator assigned to loading and operation. It also reports a 99.8% first-pass inspection result under the customer’s stated weld-length sampling method. These are application-specific reported results, not a performance guarantee for other vessel designs.
Fit-up still matters
Seam tracking compensates for position changes; it does not remove the need for controlled joint fit-up. Shell roundness, half-pipe contact, shielding, material condition and the qualified welding procedure must be evaluated during trials.
Request an application review
Send reactor and head drawings, half-pipe size, material, wall thickness, total weld length, inspection requirements and target cycle time.
haibao robot
Shao Yicheng · Key Account Project Director · International Welding Engineer (IWE)
Email: masterhyper@163.com
Phone / WhatsApp: +86 177 5158 3908
Office: +86 519 8837 0688
RELATED NEWS
- 3D Laser Cutting for Fitness Equipment Frames | haibao robot 2026-11-01
- Automated 3D Laser Trimming for Hot-Stamped Steel | haibao robot 2026-11-01
- Laser Trimming and Hole Cutting for Bent Tubes | haibao robot 2026-11-01
- Large-Format 3D Laser Cutting for Long Metal Parts | haibao robot 2026-11-01
- 3D Laser Cutting for Hydroformed Automotive Tubes | haibao robot 2026-11-01
Categories
Latest News
Contact Us
Contact: Mr.Shao
Phone: 0086-17751583908
E-mail: 691043690@qq.com
Whatsapp:86-17751583908
Add: shanghai, China TianHe District, GuangZhou Num 899