Elevated Longitudinal Seam Welder for Tank Shells
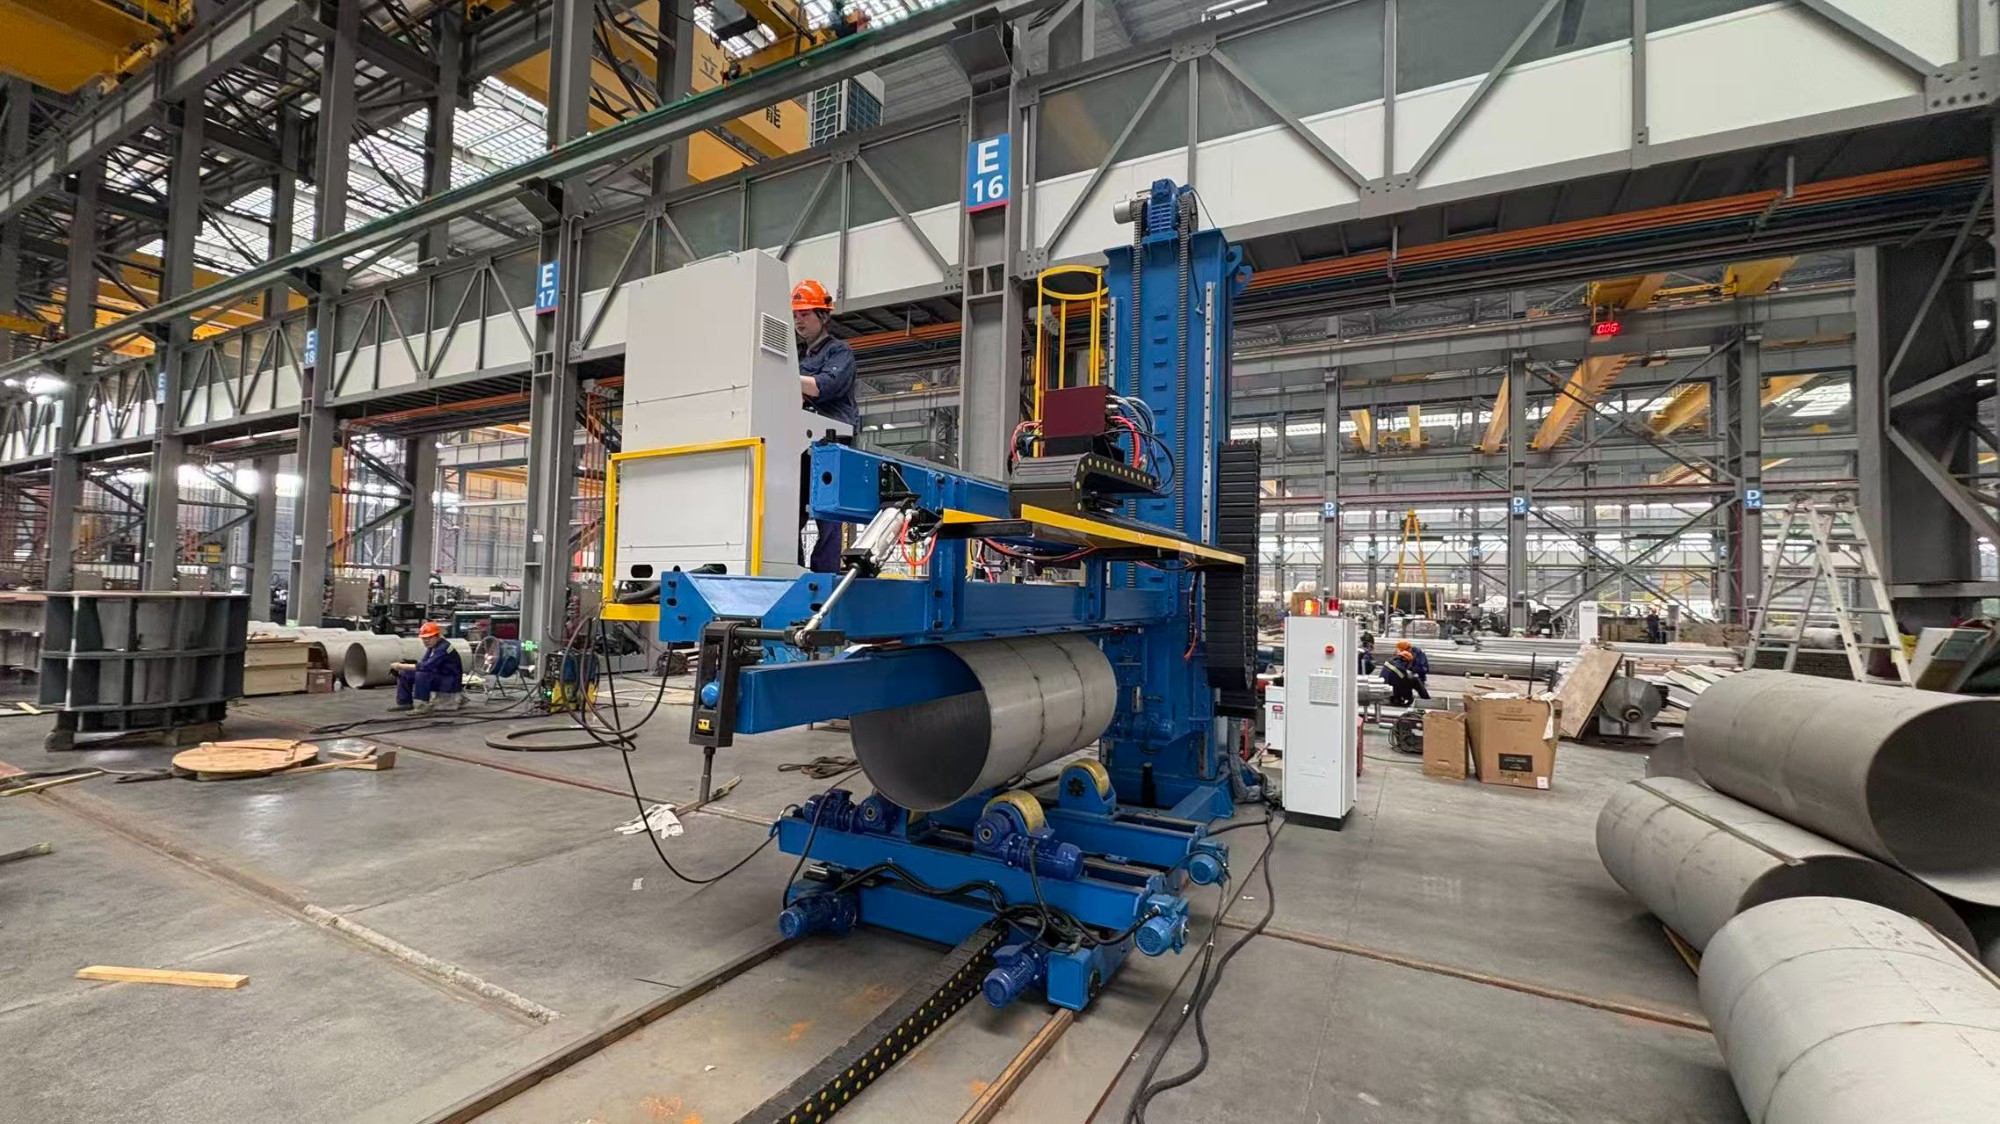
Piano-key longitudinal seam welding for cylindrical shells, with an elevated platform and shell handling arrangement sized for vessel fabrication.
Equipment and application images

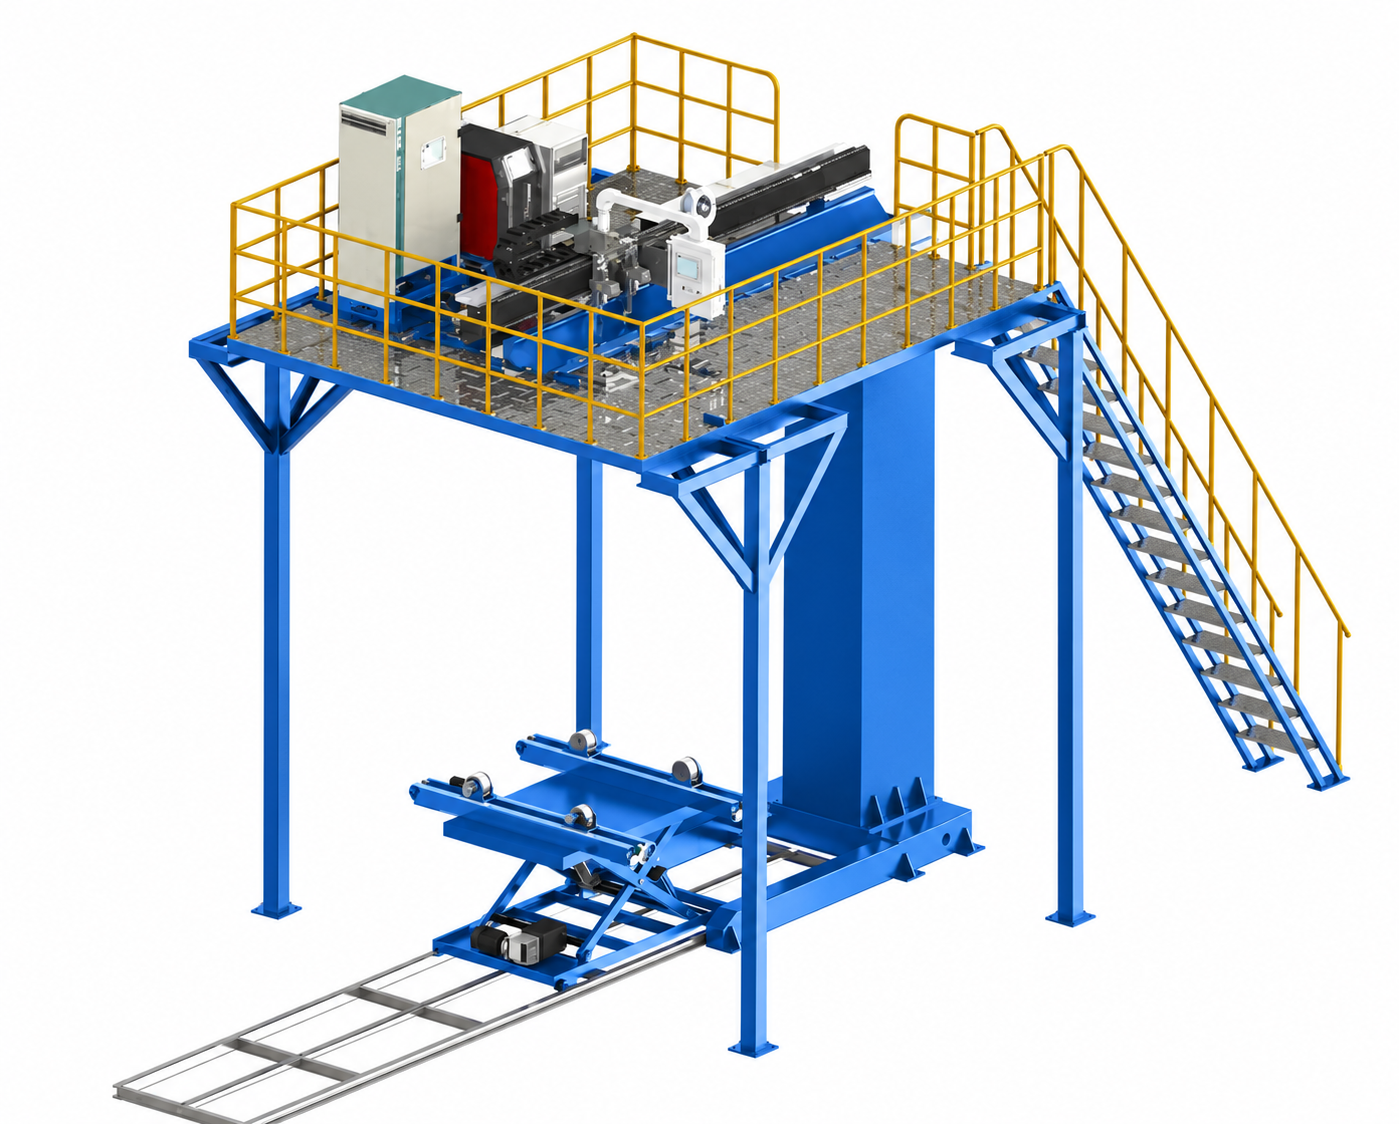
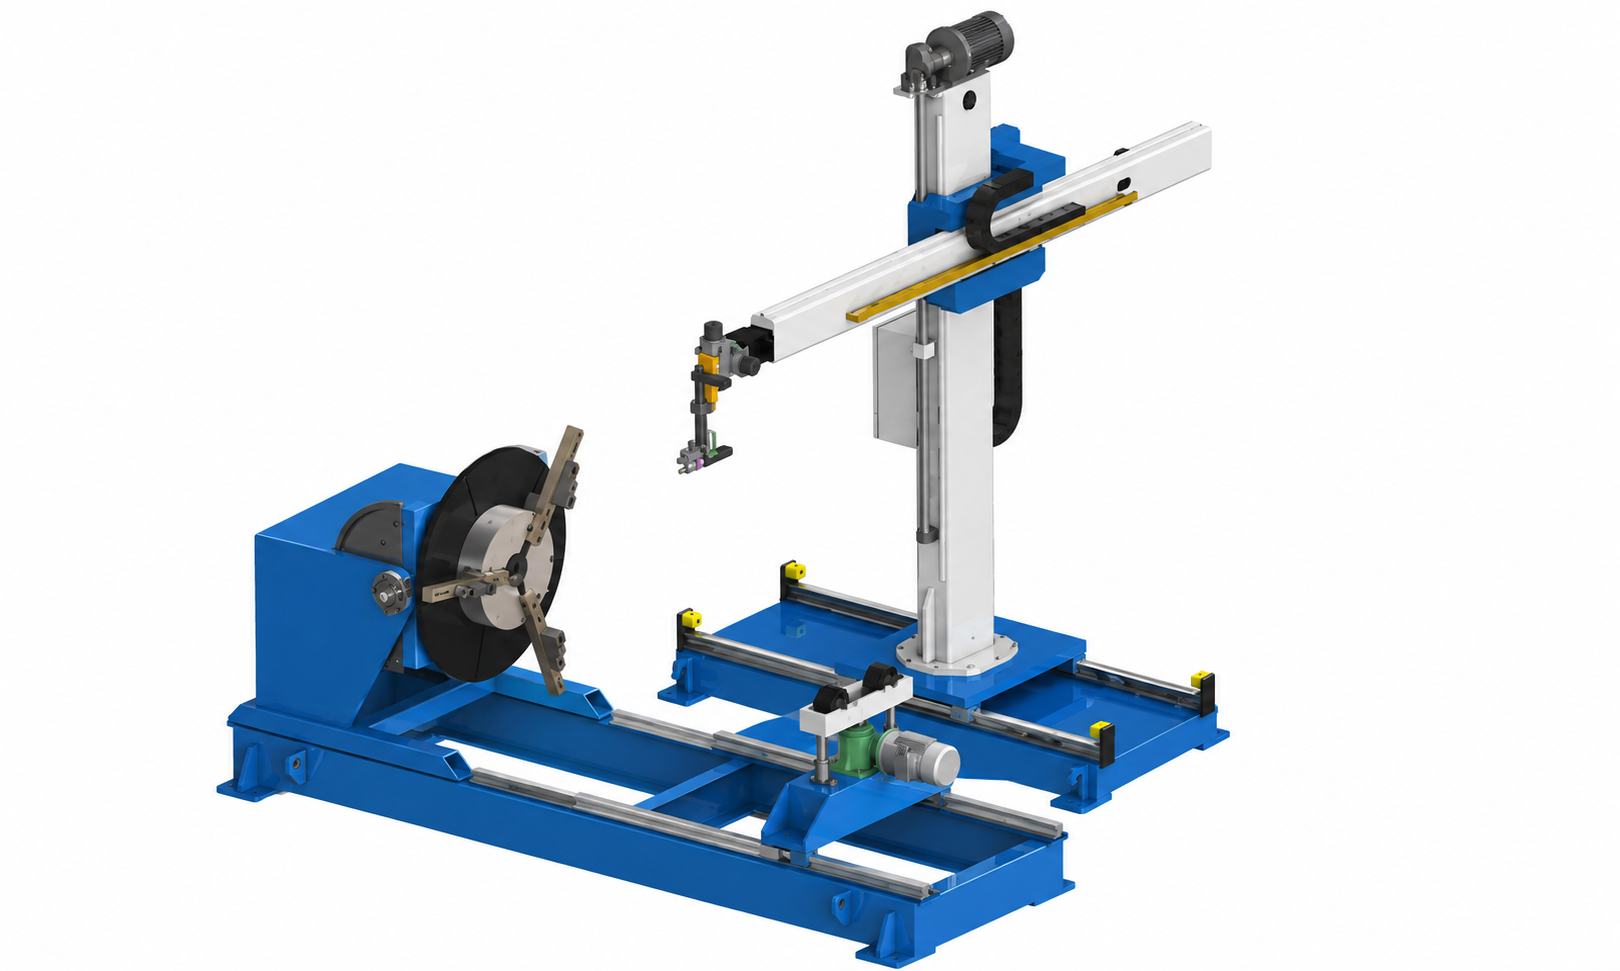
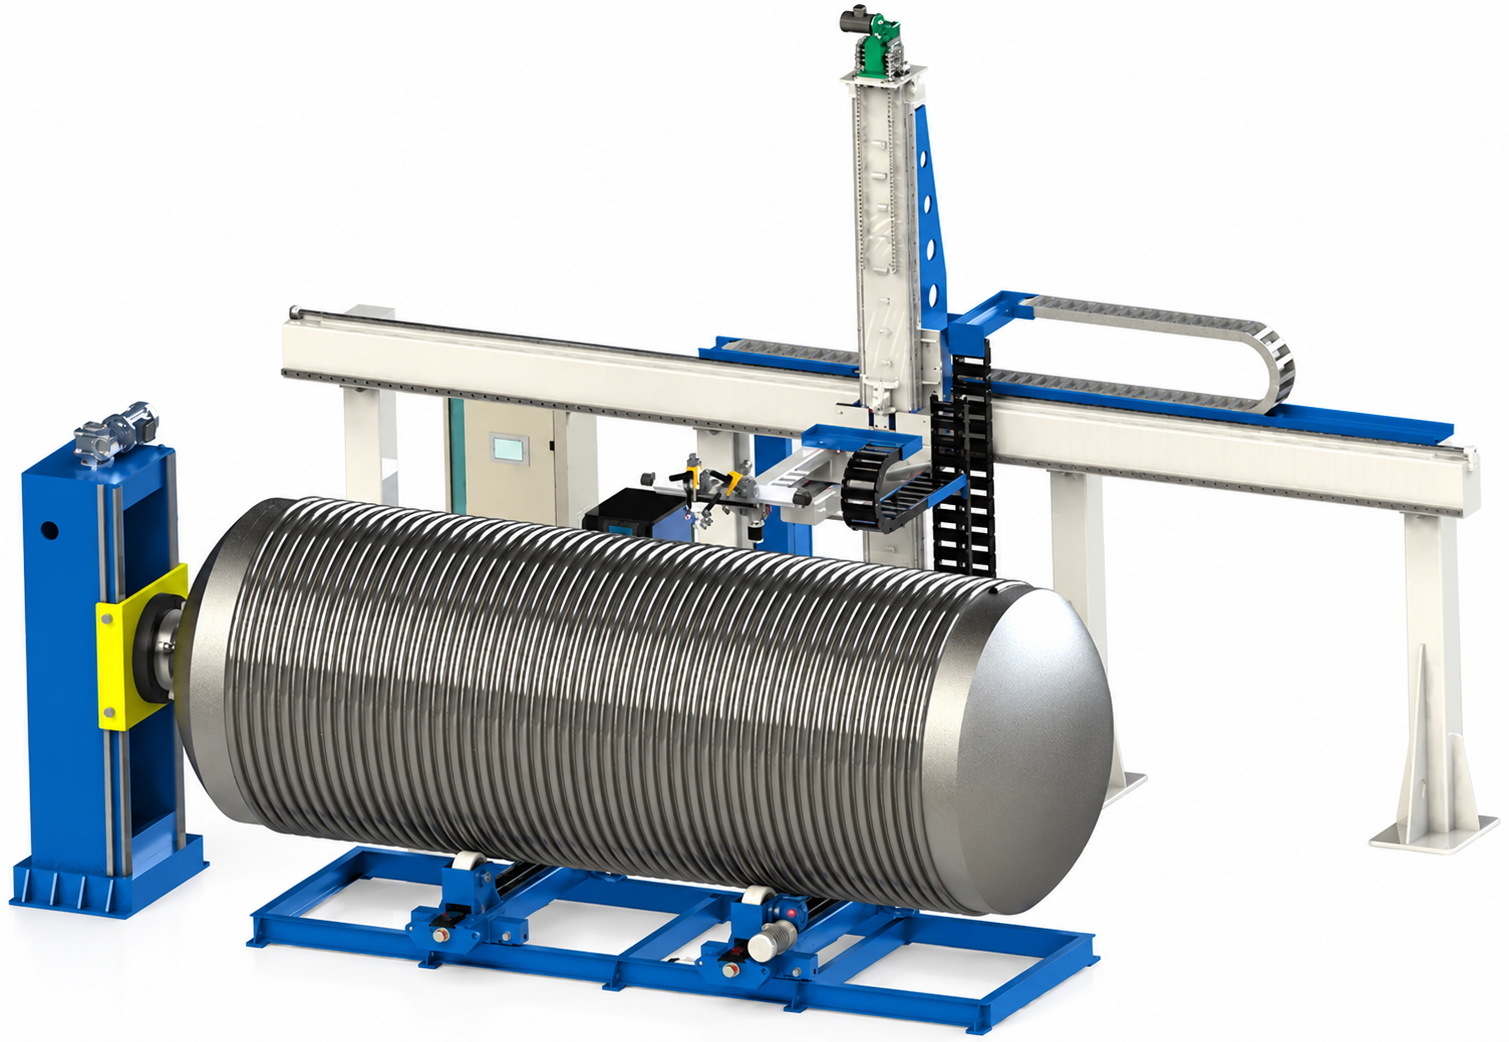
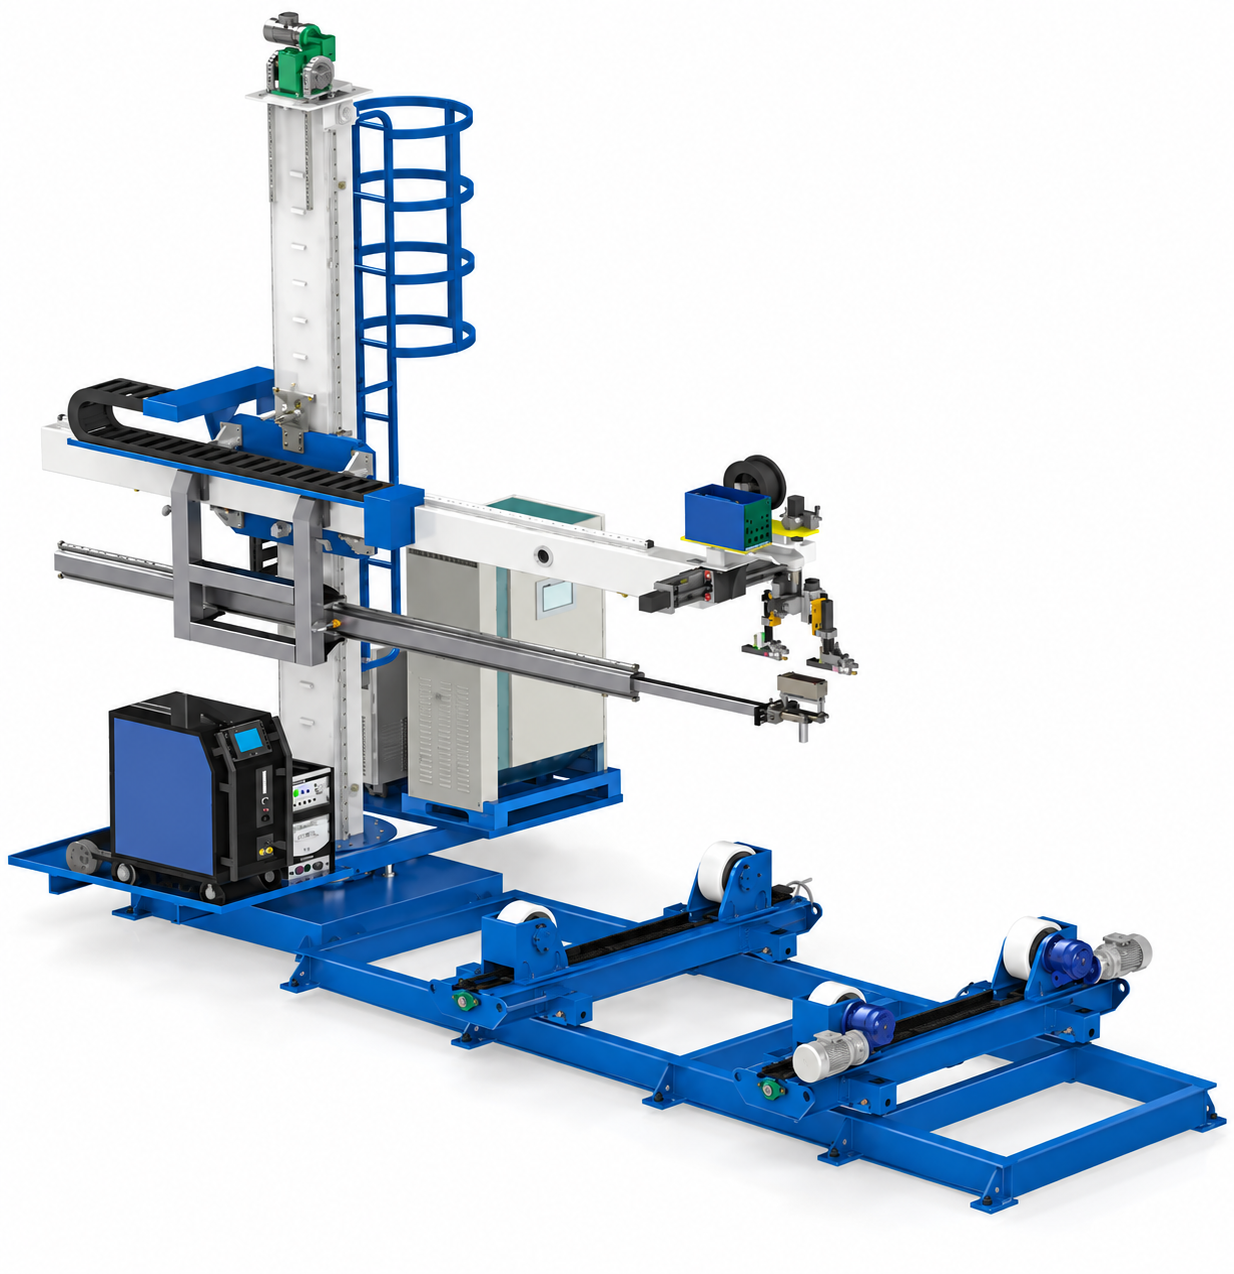
CAD configuration illustration. Final equipment follows the agreed technical scope.

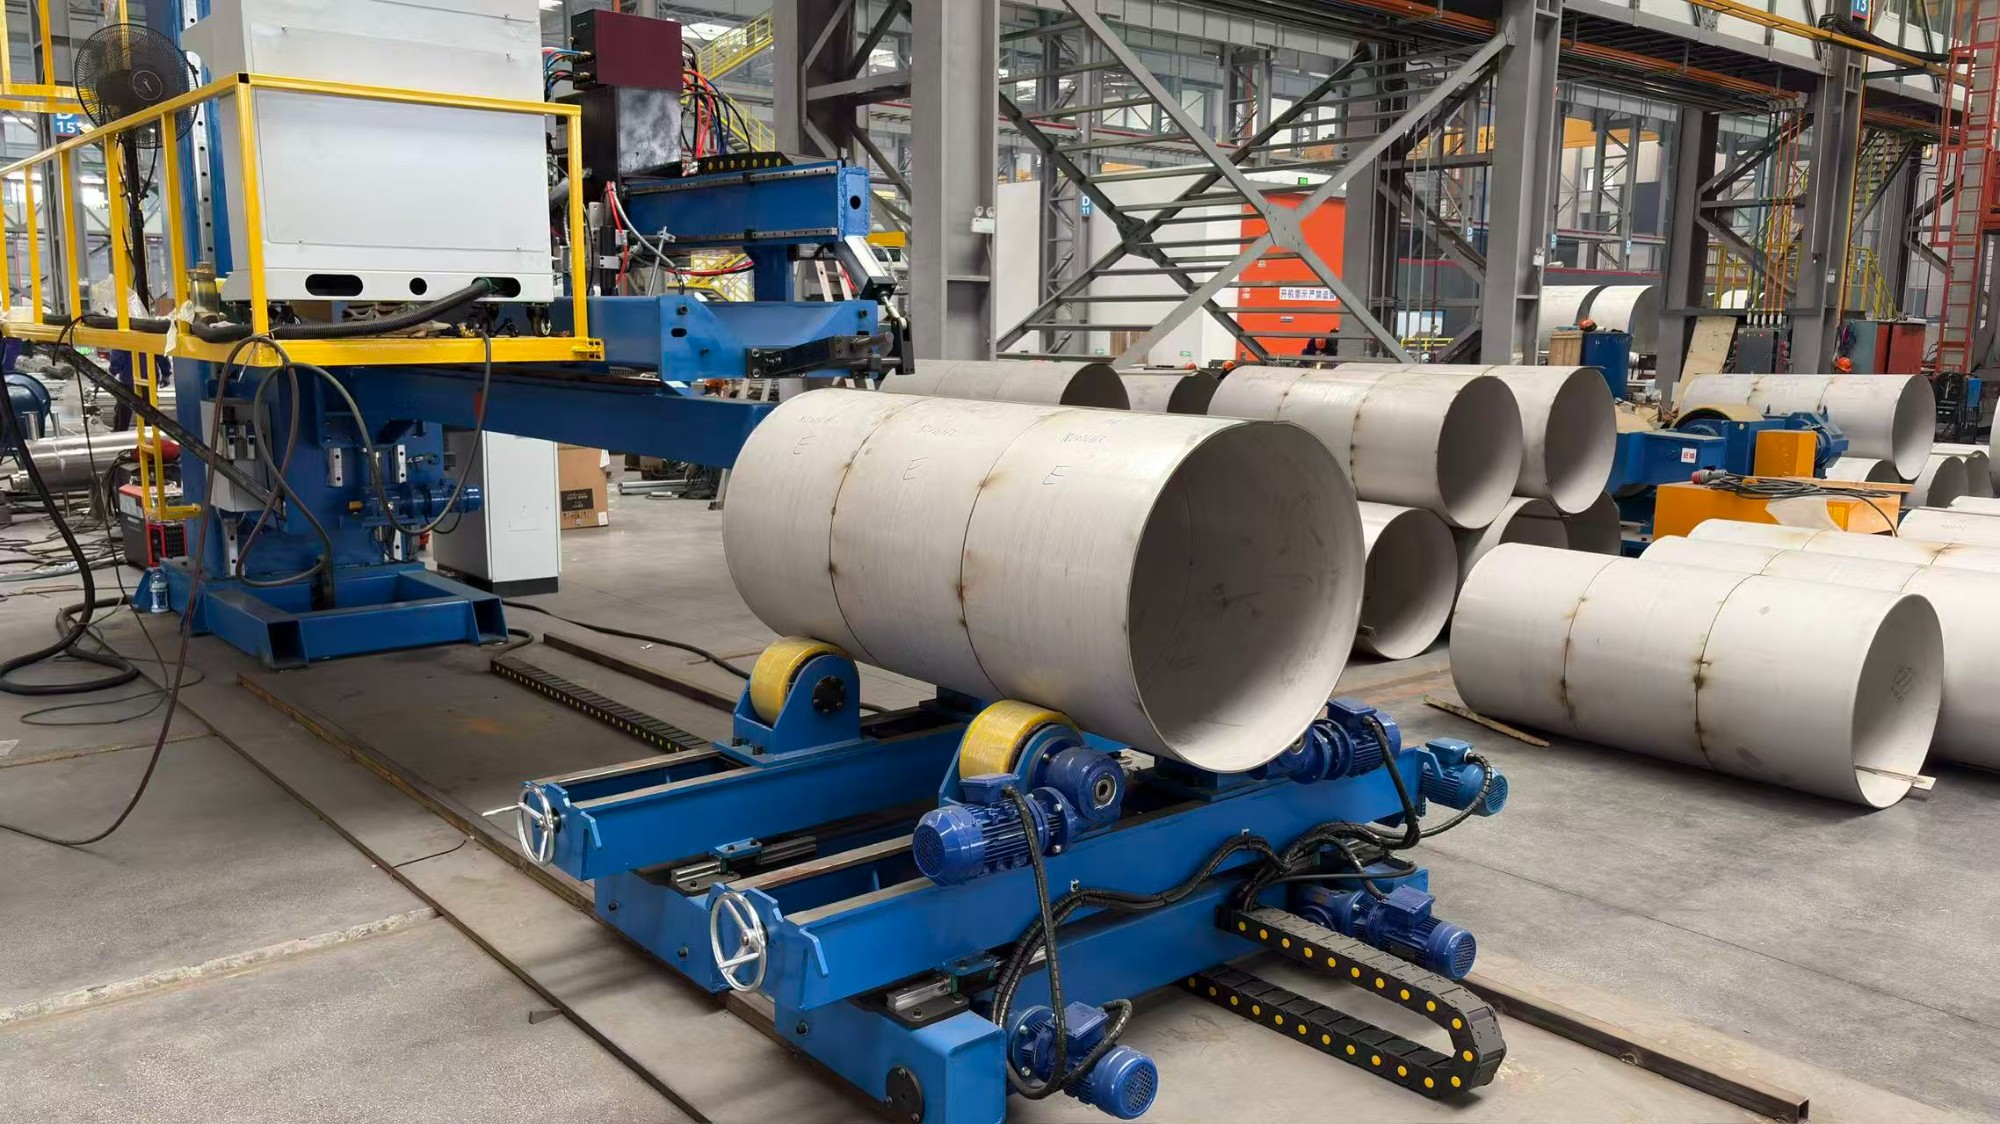
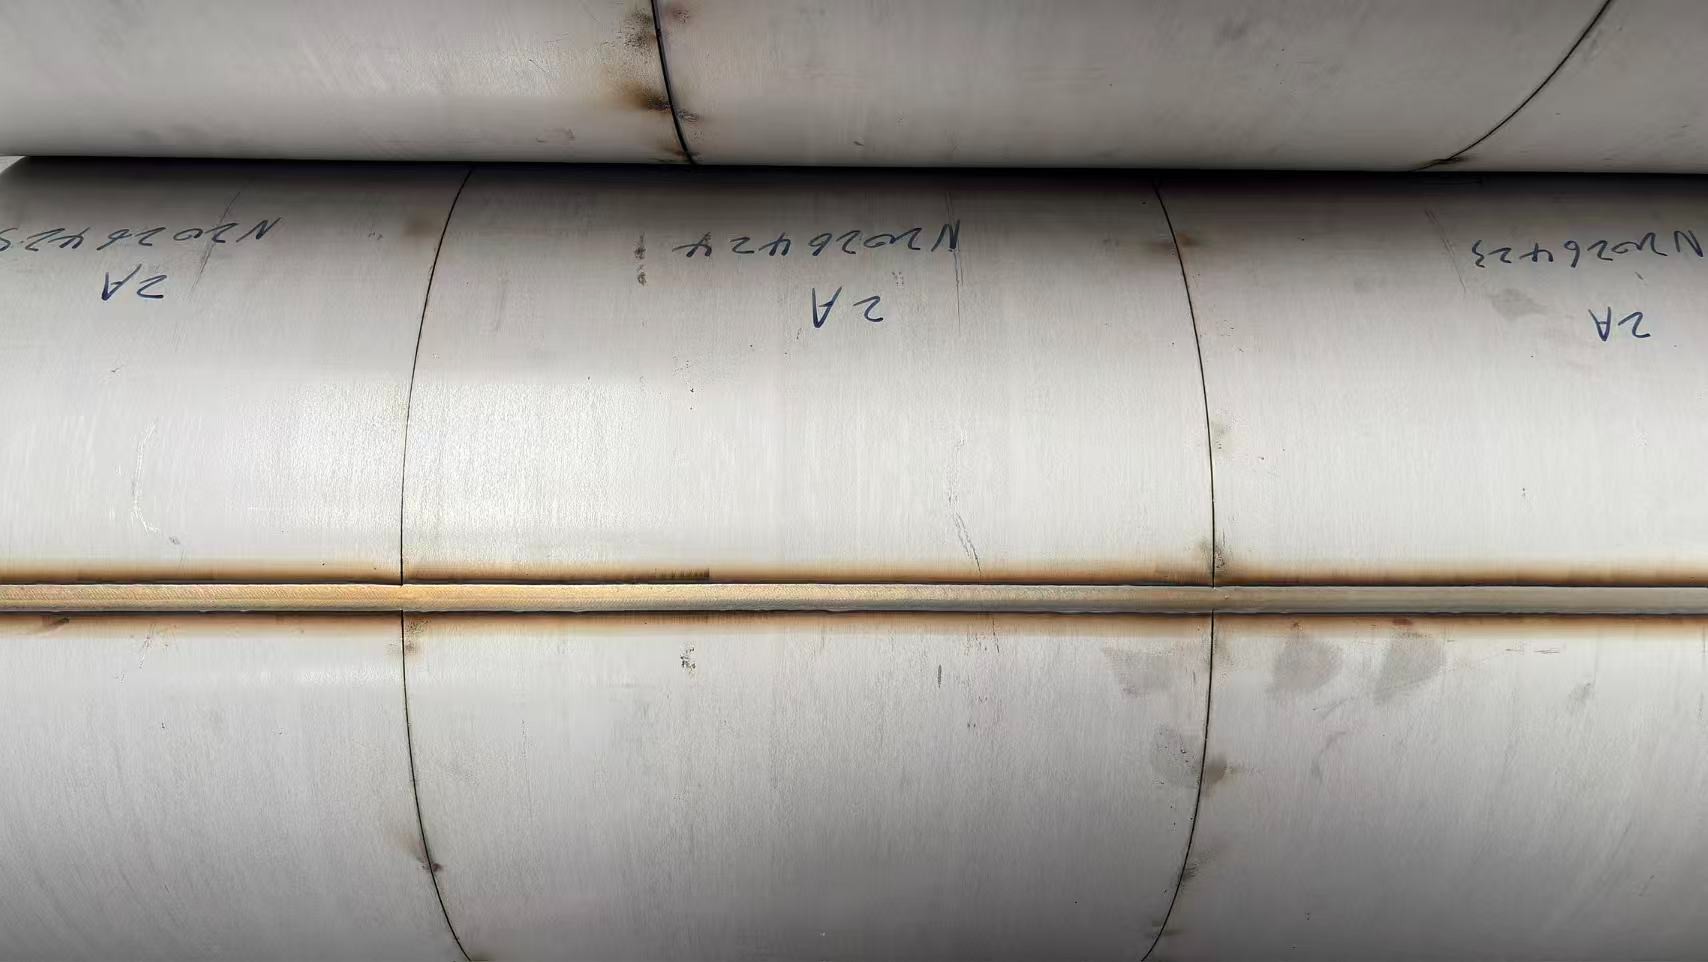
Welding application reference. Results depend on material and welding procedure.

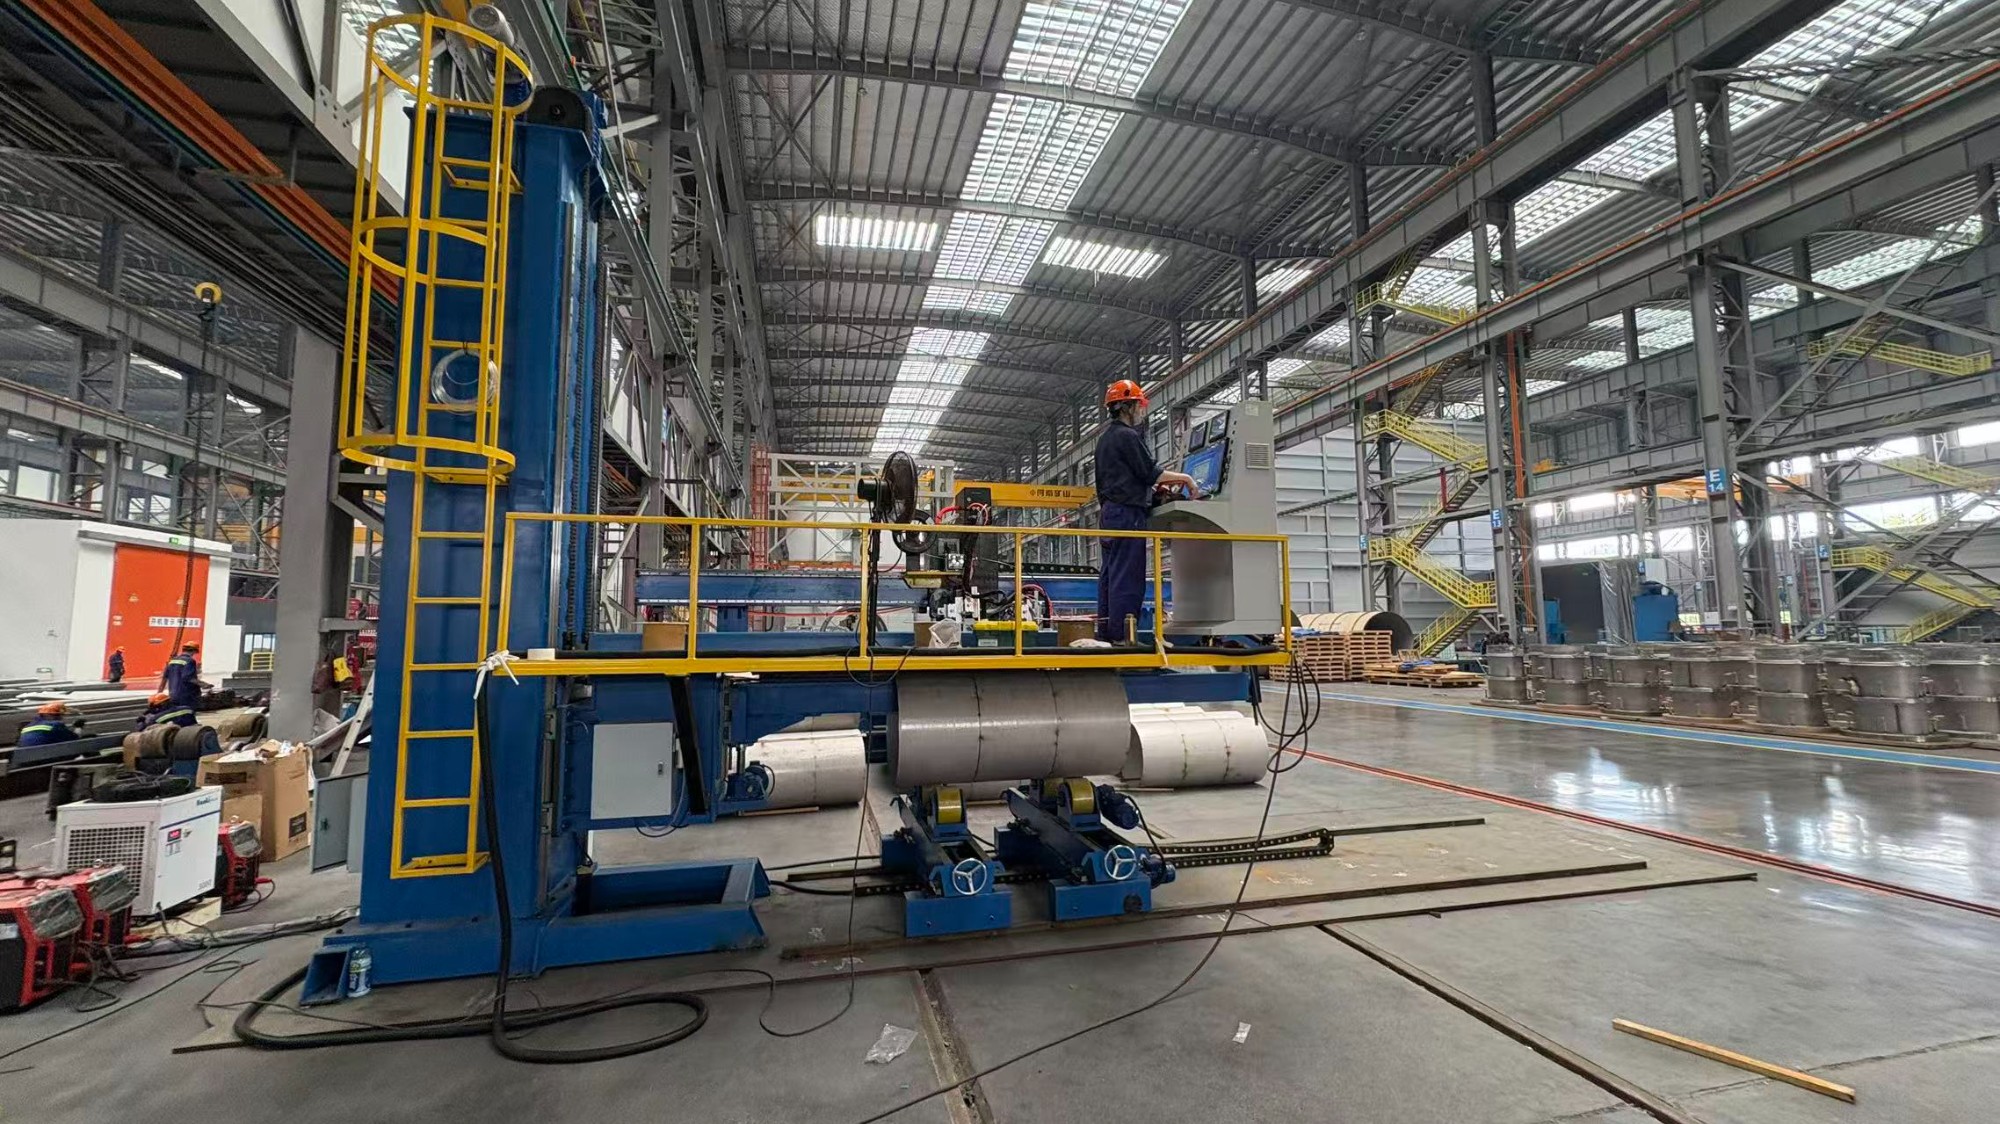
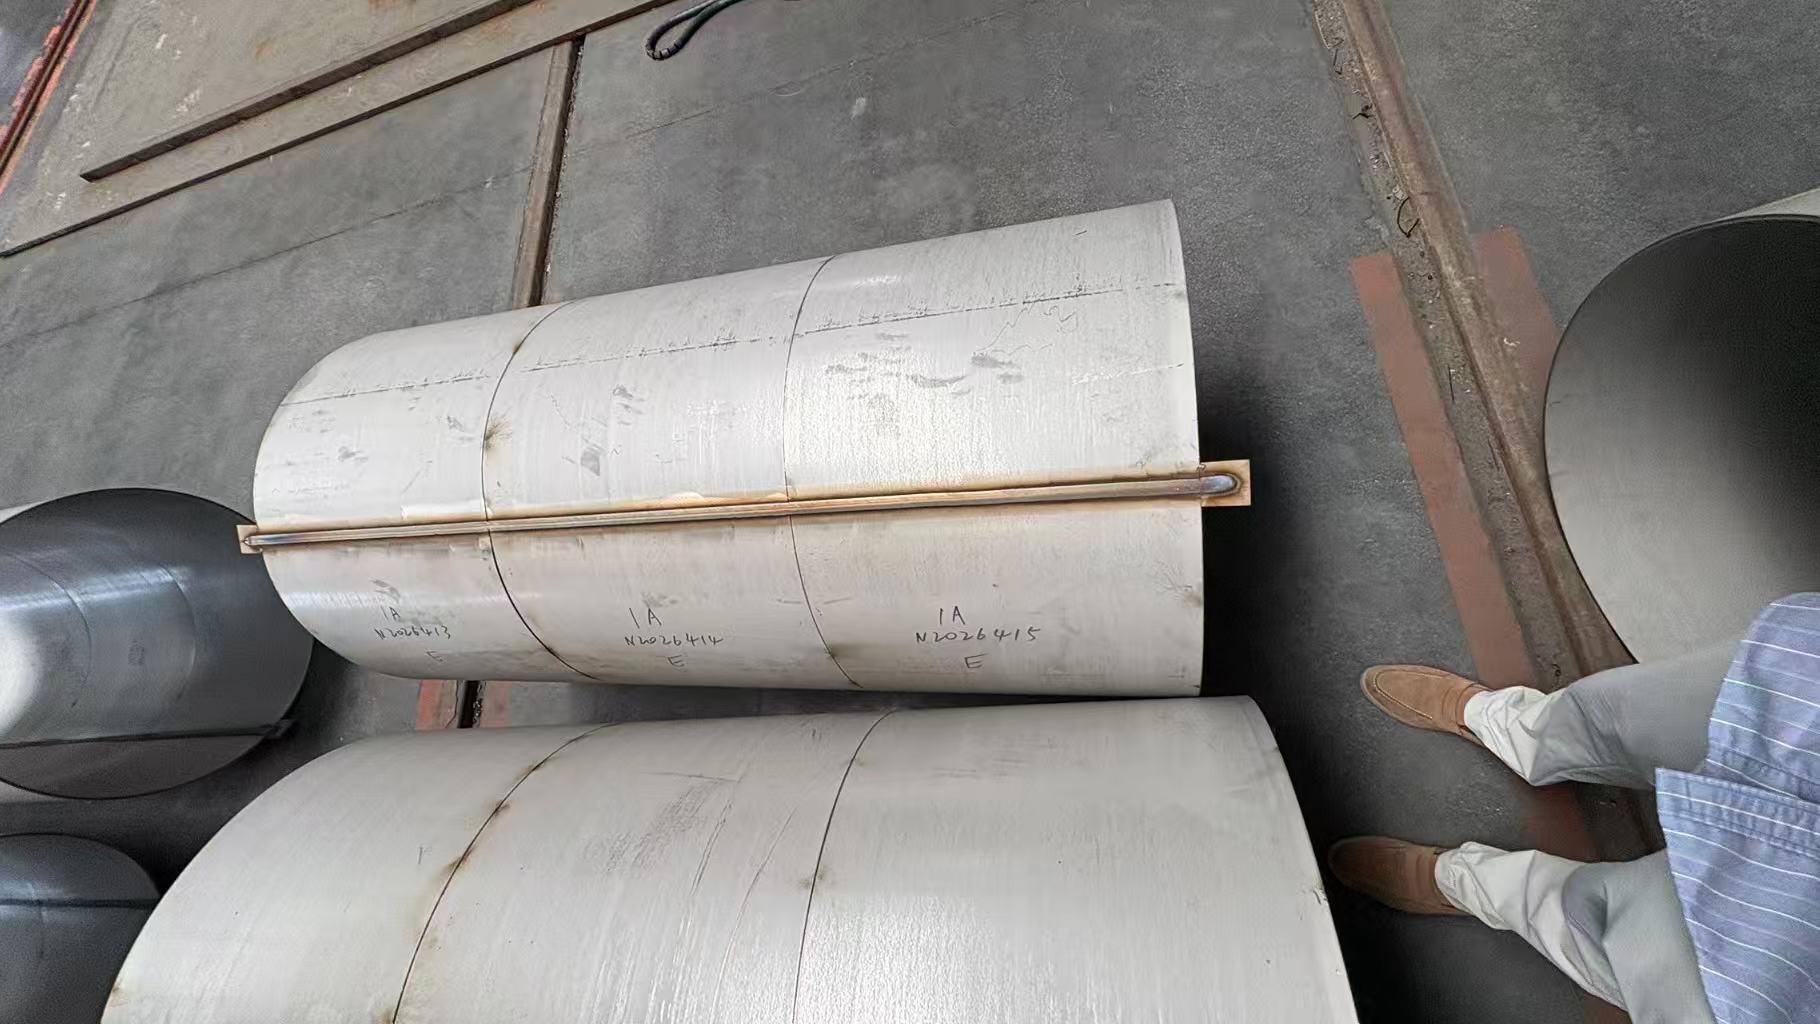
Welding application reference. Results depend on material and welding procedure.

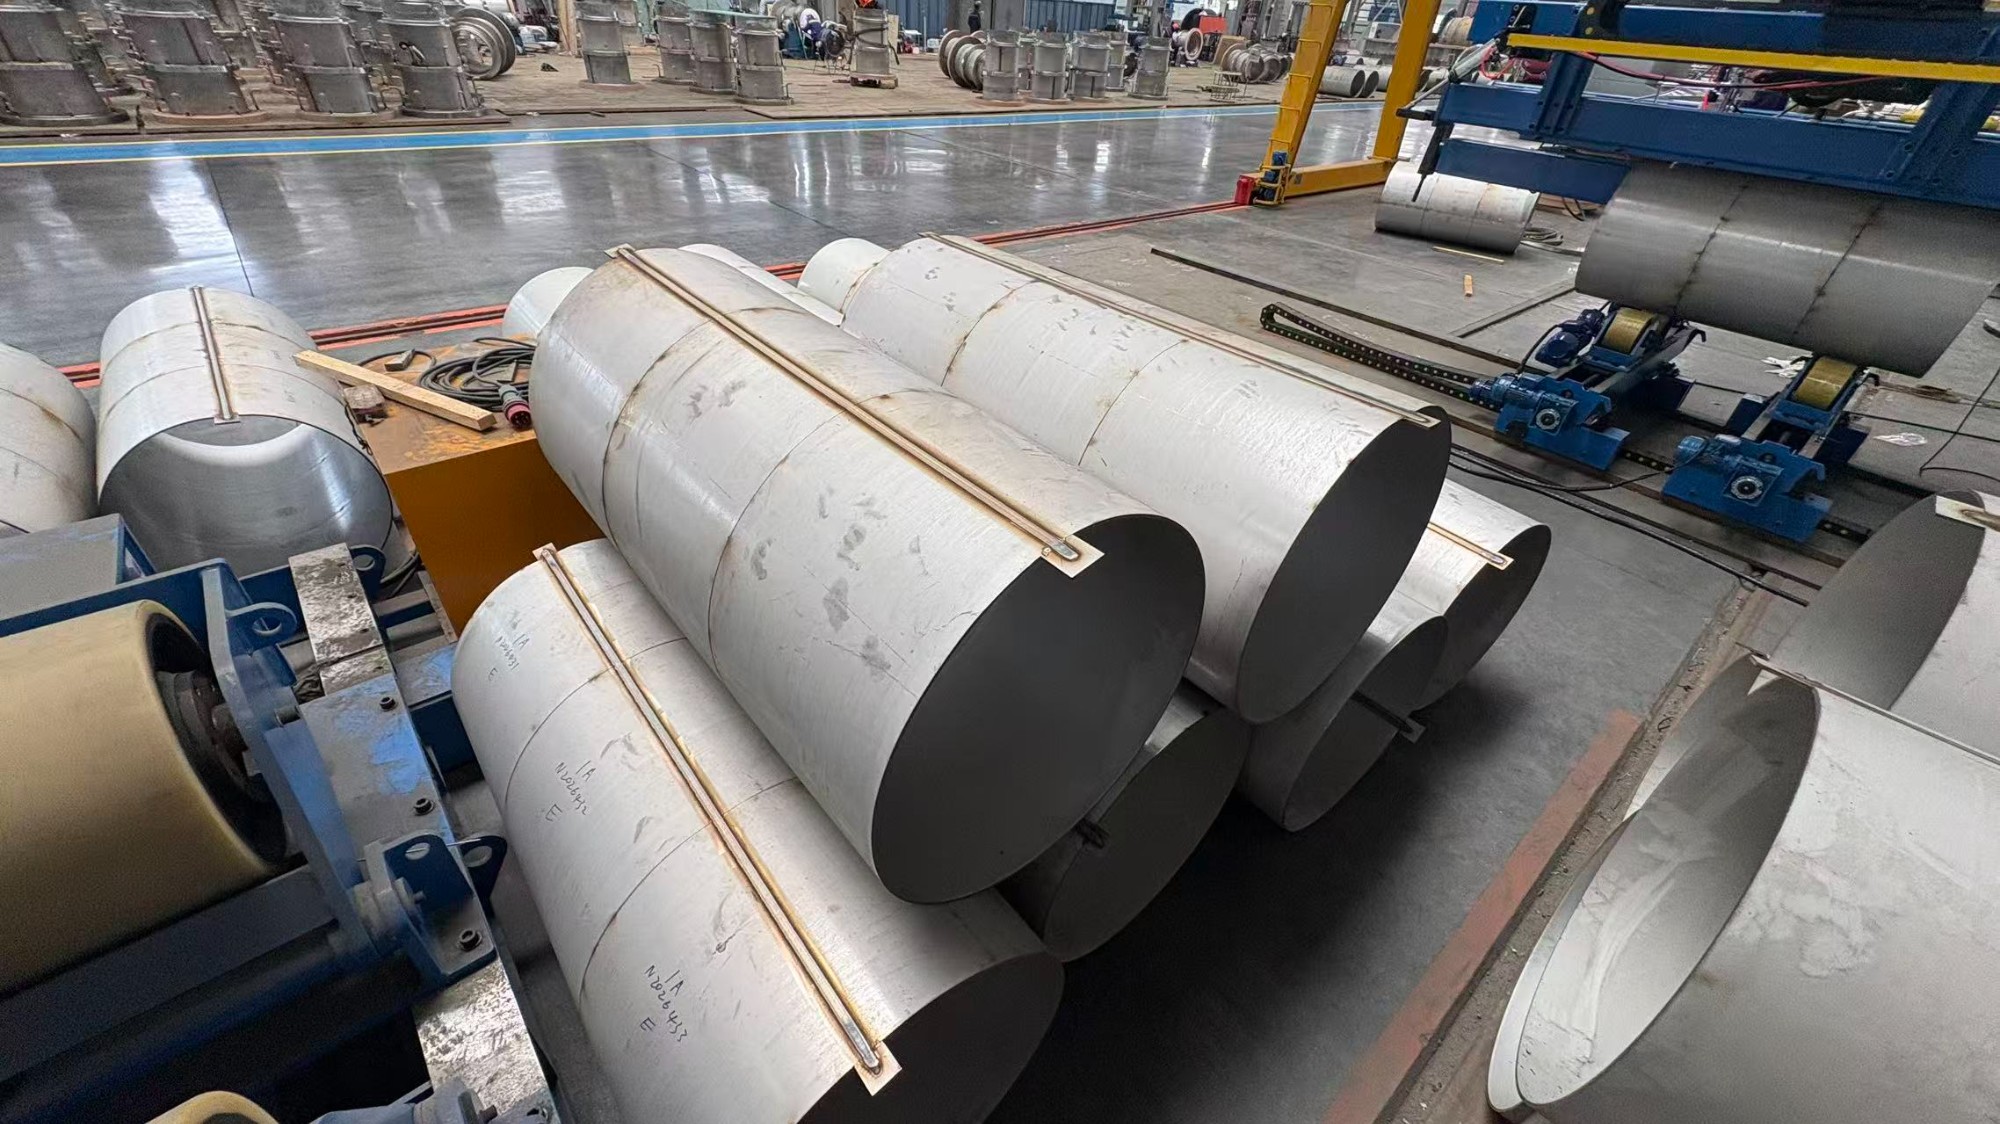
Welding application reference. Results depend on material and welding procedure.

Welding application reference. Results depend on material and welding procedure.

Welding application reference. Results depend on material and welding procedure.

Welding application reference. Results depend on material and welding procedure.
Elevated Longitudinal Seam Welder for Tank Shells
haibao robot supplies piano-key longitudinal seam welding for cylindrical shells, with an elevated platform and shell handling arrangement sized for vessel fabrication.
How the system works
Opposed piano-key clamps align and restrain the shell edges while the torch traverses the longitudinal seam. A backing arrangement supports the joint and can provide shielding and heat removal. The elevated layout accommodates the shell and provides access to the welding station.
Configuration and selection data
| Joint | Internal or external longitudinal shell seam |
|---|---|
| Clamping | Piano-key pressure fingers |
| Nominal thickness range | 0.5–10 mm, process and material dependent |
| Processes | TIG, MIG/MAG, plasma or SAW options |
| Applications | Tanks, process vessels, large tubes and fabricated shells |
| Platform and loading | Customized to shell diameter, length and factory layout |
The thickness range is a fixture selection reference, not a promise of single-pass penetration. Backing, shielding, fit-up and the welding procedure must be matched to the material.
Match the process to the workpiece
Material grade, wall thickness, joint design, fit-up and inspection requirements determine the welding package. TIG (GTAW), MIG/MAG (GMAW), plasma arc welding (PAW) and submerged arc welding (SAW) use different power sources, torches and consumables. Select the required process during application review; options listed on this page are not all included in one standard machine.
What is included in a proposal?
The proposed scope should identify the machine layout, fixtures, welding package, controls, workpiece handling and any tracking or shielding options. Confirm utilities, loading method, installation space and acceptance criteria before ordering. CAD images illustrate a configuration; actual equipment and accessories follow the agreed technical scope.
Request an application review
Send haibao robot a workpiece drawing, material grade, thickness, diameter or width, length and maximum weight. Include joint details, required output, preferred welding process and weld inspection criteria. Photos of your current loading and welding arrangement help us assess access and handling.
Request a configuration and quotation using the inquiry form below.
INQUIRY
Categories
Latest News
Contact Us
Contact: Mr.Shao
Phone: 0086-17751583908
E-mail: 691043690@qq.com
Whatsapp:86-17751583908
Add: shanghai, China TianHe District, GuangZhou Num 899