News
Half-Pipe Forming & Spiral Winding Machine | haibao robot
Project photographs and equipment references
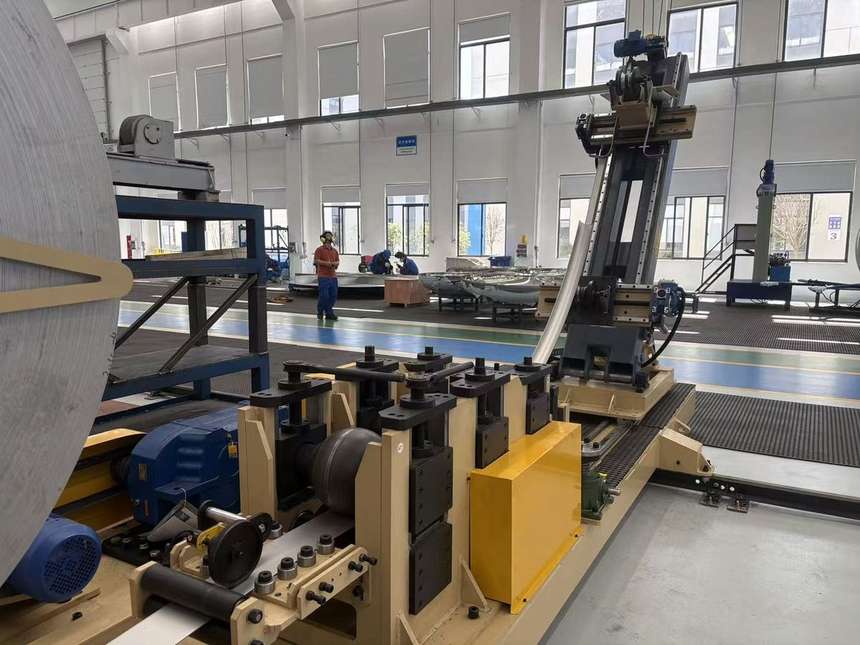
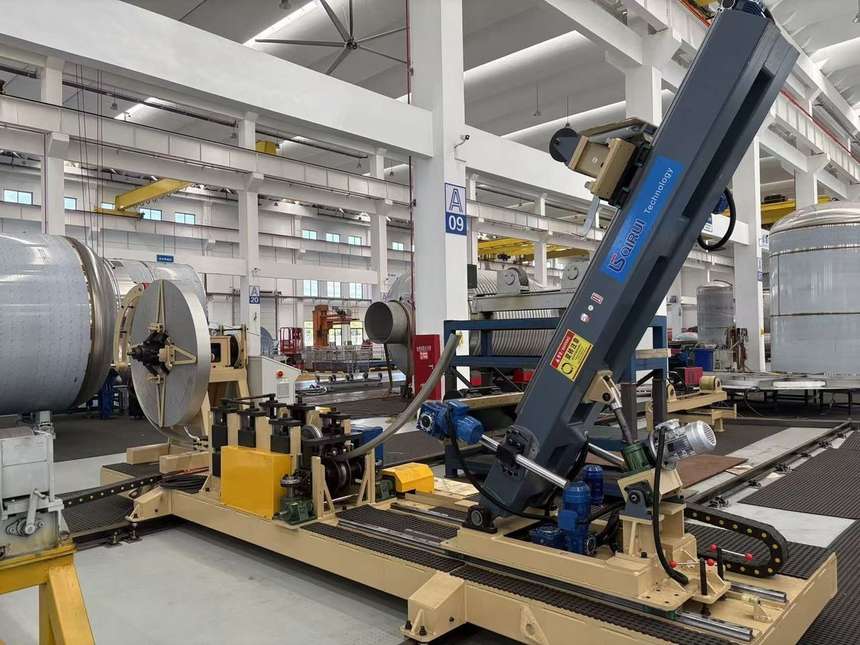
Complete half-pipe forming and winding line |
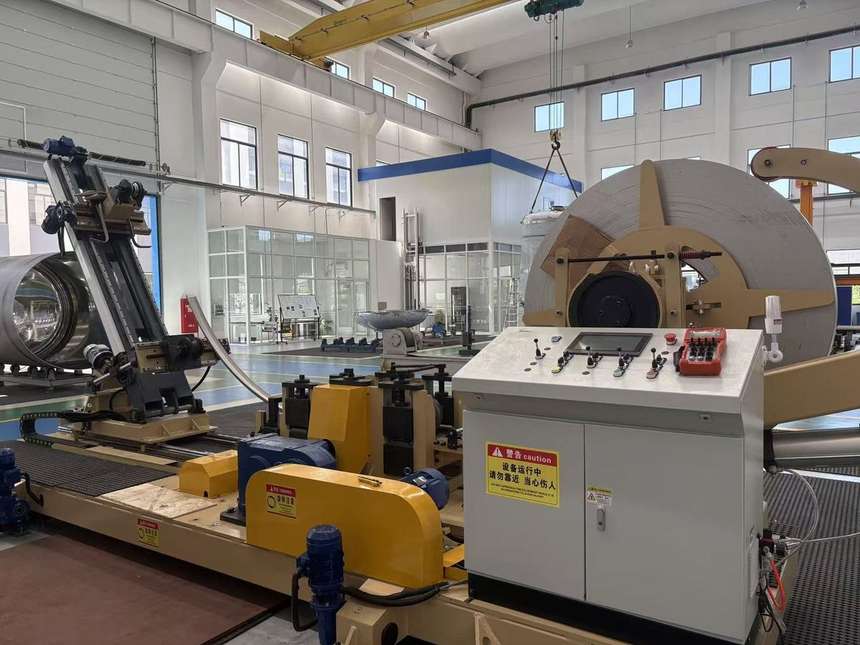
Machine bed, forming head and control station |
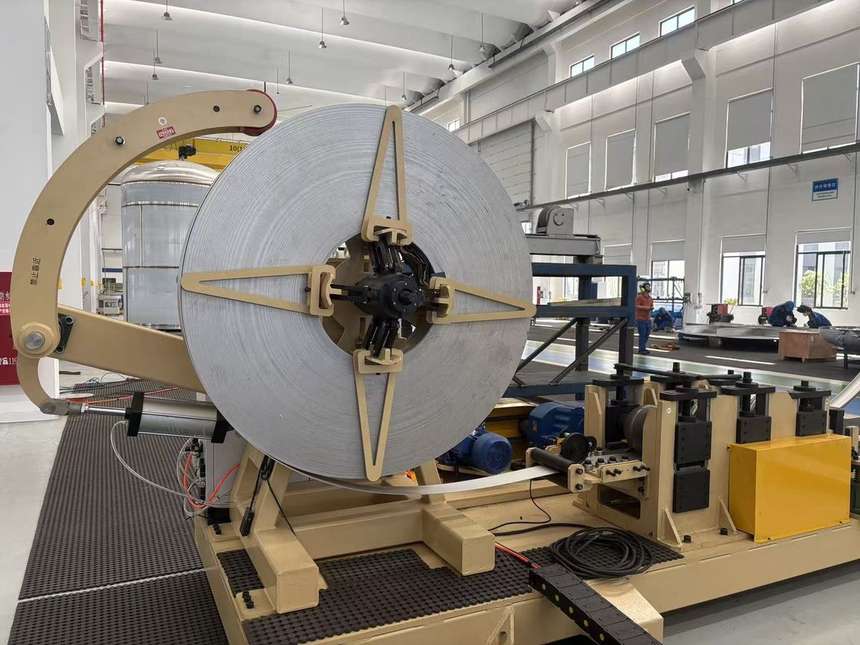
Coil decoiler and strip feeding rollers |
Tilting forming head and linear slide |
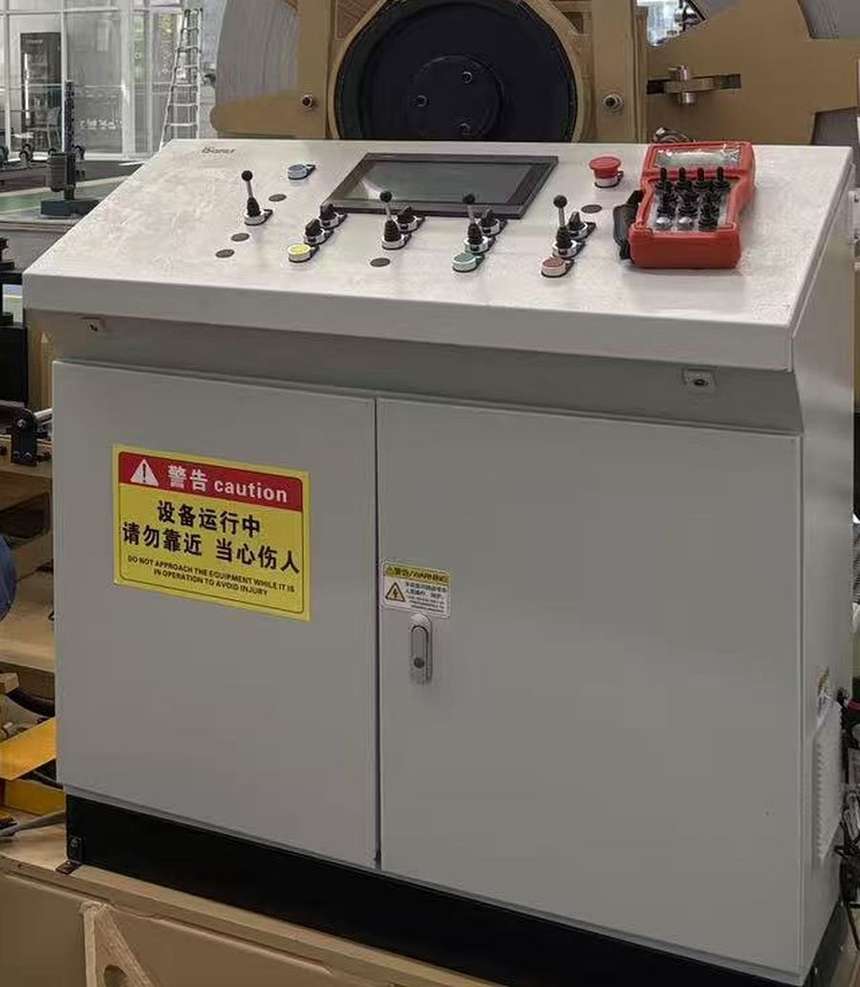
PLC touchscreen and operator controls |
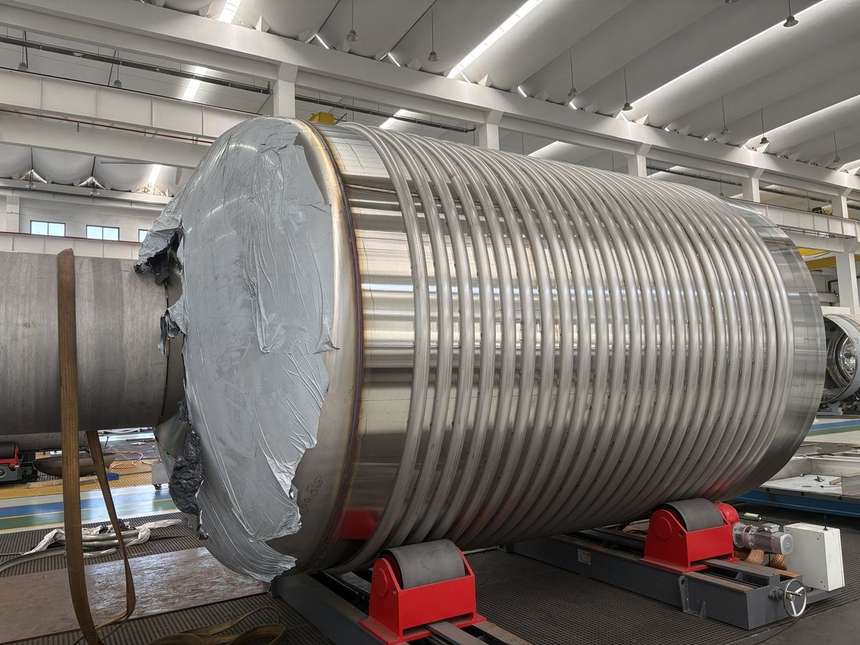
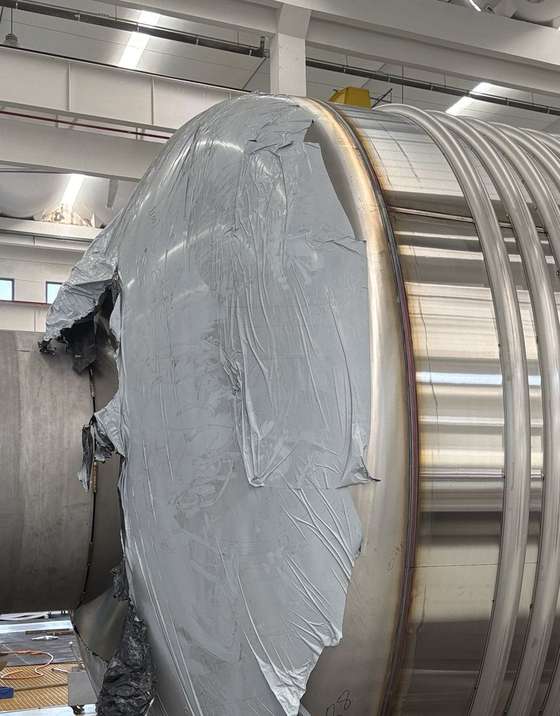
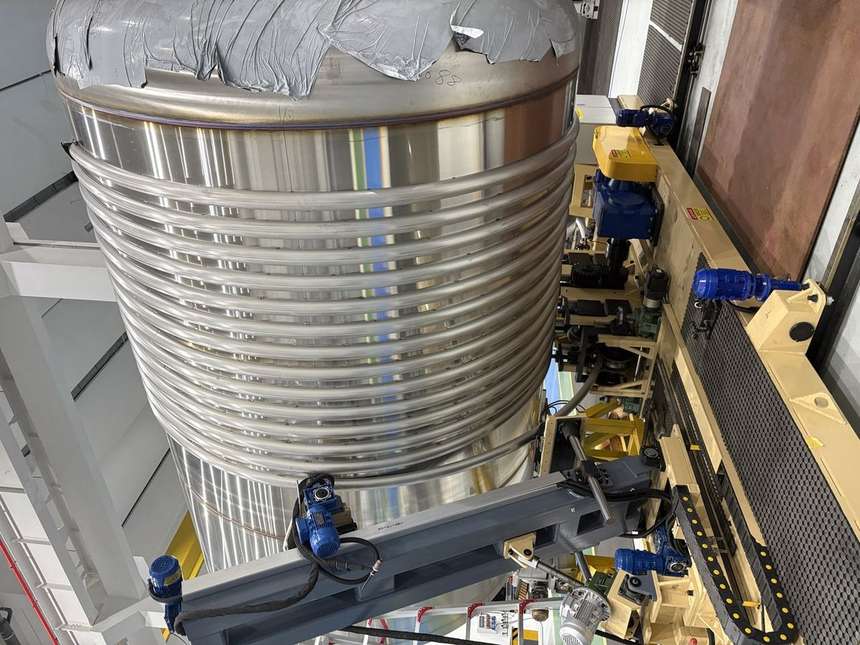
Vessel shell with a spiral half-pipe jacket |
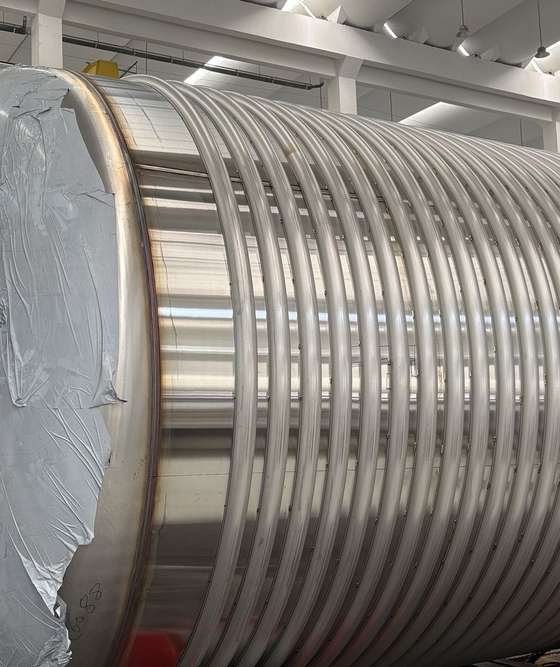
Half-pipe winding detail |
Jacket termination near the vessel head |
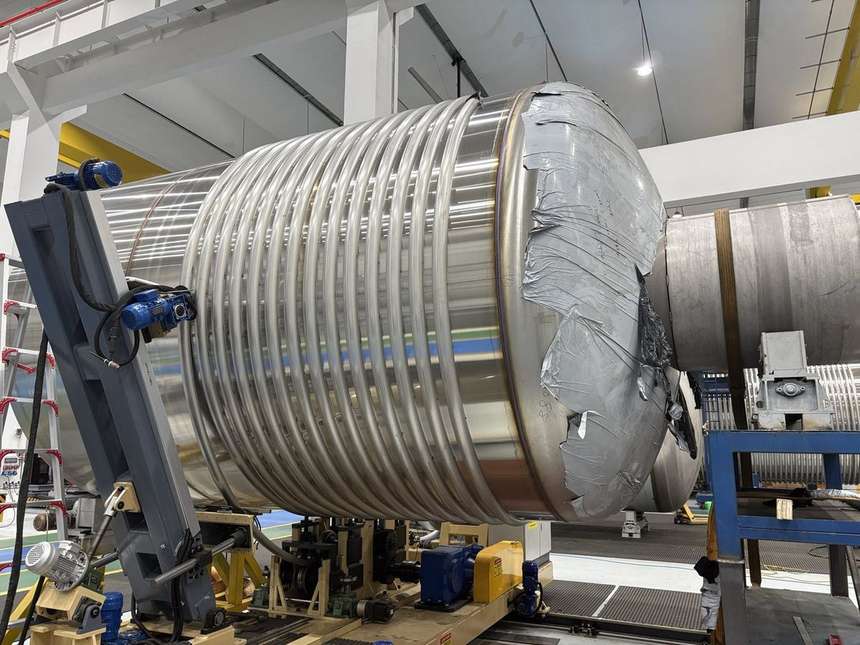
Forming head beside the rotating shell |
Completed spiral jacket on the vessel shell |
haibao robot · CUSTOMER APPLICATION
Continuous Half-Pipe Jacket Forming for Pressure Vessels
Anhui Saide Qirui required a complete line for forming and winding half-pipe jackets on pressure vessel shells. haibao robot integrated strip preparation, progressive forming and spiral winding into a coordinated production system.
The production challenge
Making a jacket from separate rolled sections requires repeated fit-up, alignment and joining. Pitch variation and gaps between the half-pipe and shell add work for the welding team. The project brought strip feeding, forming and winding onto one common machine bed.
An integrated forming line
haibao robot supplied decoiling, leveling, multi-roll preforming, a tilting forming head, spiral winding, variable-speed rotation supports and PLC controls. The forming head travels along linear guides while axial feed and vessel rotation establish the winding pitch. Head height and angle can be adjusted for different shell diameters.
Material handling and control
A four-jaw expanding mandrel holds the coil. A following pressure arm stabilizes strip delivery, and driven rollers progressively form the half-round section. Operators set feed, rotation and pitch from the touchscreen, with manual positioning for setup and an automatic cycle for production. Roller profiles, pressure and speed must be matched to material springback.
Typical application range
The published equipment range covers vessel diameters of 600–4,000 mm and lengths up to 6,000 mm, half-pipe outside diameters of 25–120 mm and strip thicknesses of 1.5–4.0 mm. Carbon steel, stainless steel and duplex stainless steel are considered during process selection. These are typical ranges, subject to workpiece review and the technical agreement.
Delivery and reported results
Delivery included the machine, electrical controls, installation, commissioning, material trials and operator training. The project report records successful initial material trials and customer feedback on consistent pitch, close shell contact and less fitting and grinding before welding. After forming, the jacket is positioned and welded under the specified fabrication and inspection procedure.
Request an application review
Send vessel diameter and length, half-pipe size, strip material and thickness, required pitch and production volume.
haibao robot
Shao Yicheng · Key Account Project Director · International Welding Engineer (IWE)
Email: masterhyper@163.com
Phone / WhatsApp: +86 177 5158 3908
Office: +86 519 8837 0688
RELATED NEWS
- 3D Laser Cutting for Fitness Equipment Frames | haibao robot 2026-11-01
- Automated 3D Laser Trimming for Hot-Stamped Steel | haibao robot 2026-11-01
- Laser Trimming and Hole Cutting for Bent Tubes | haibao robot 2026-11-01
- Large-Format 3D Laser Cutting for Long Metal Parts | haibao robot 2026-11-01
- 3D Laser Cutting for Hydroformed Automotive Tubes | haibao robot 2026-11-01
Categories
Latest News
Contact Us
Contact: Mr.Shao
Phone: 0086-17751583908
E-mail: 691043690@qq.com
Whatsapp:86-17751583908
Add: shanghai, China TianHe District, GuangZhou Num 899